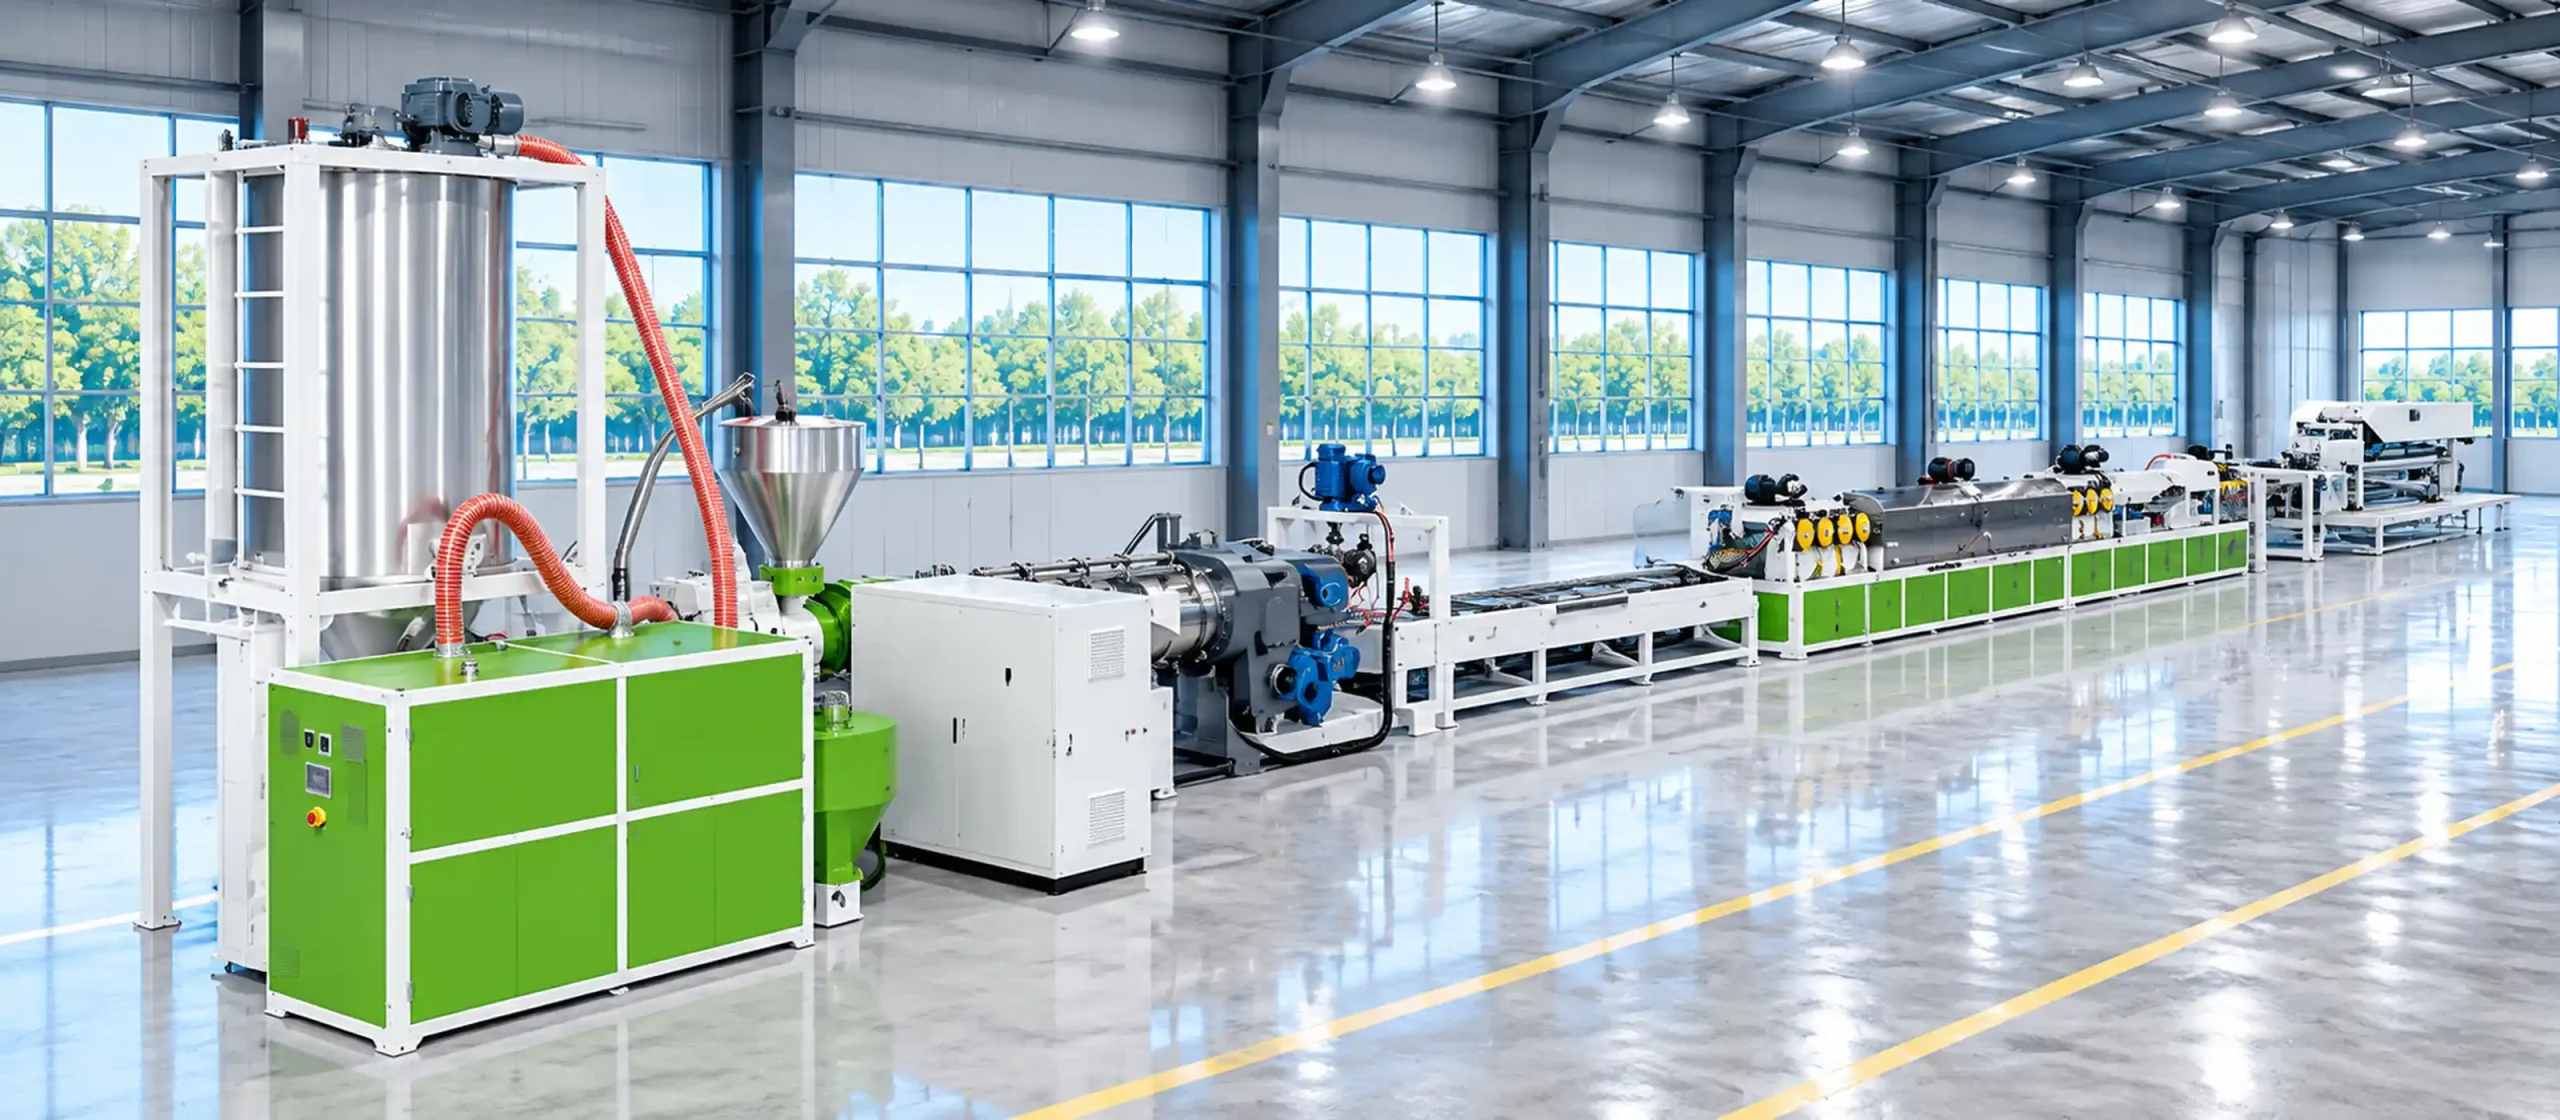
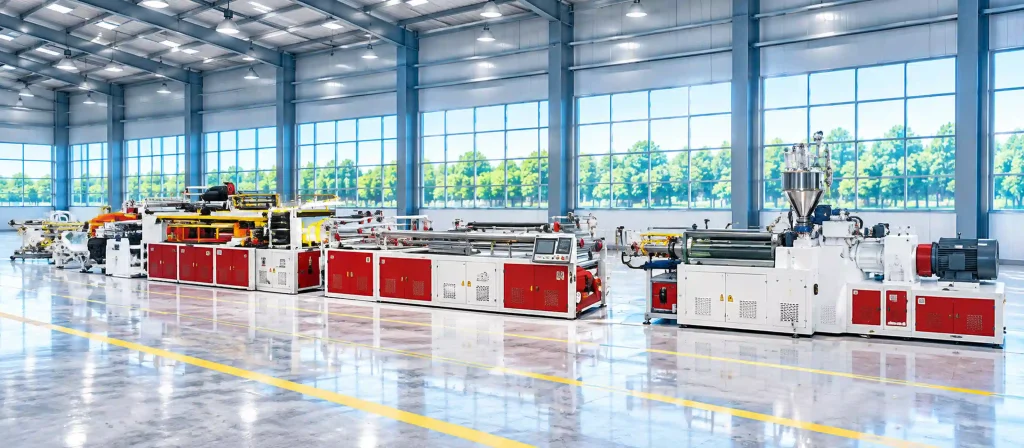
WPC Flooring Production Line
Jwell WPC Flooring Production Line produces lightweight, durable wood-plastic composite flooring with a foamed core, precision calendering, embossing, UV coating and automated profiling.
The PET Strapping Extrusion Line is part of JWELL’s complete extrusion portfolio. Customers evaluating this PET Strapping Extrusion Line also frequently request our PP Strapping Extrusion Line | Jwell Machinery and rPET Sheet Extrusion Line — Factory Acceptance Test, which share the same proven screw, die and control platforms. For layout drawings, pricing and lead times, contact JWELL Machinery directly.
The Jwell PET strapping line’s standard configuration extrudes 4 strands simultaneously (一出四) from a single T-die — four parallel straps traveling through a shared or individually-lane stretching oven, embossed, and wound on four independent winding stations. This 4-strand architecture delivers approximately 450 kg/h total line output (300-500 kg/h range), with each strand producing 75-125 kg/h depending on strap width and thickness.
The 4-strand configuration provides three operational advantages over running the same total output on multiple single-strand lines:
Capital efficiency: One extruder, one control system, one dryer, one operator, and one factory footprint serve all four strands. The capital cost per ton of annual PET strap capacity is approximately 30-50% lower than four single-strand lines.
Labor efficiency: One operator manages the entire 4-strand line versus four operators for four single-strand lines. In markets where skilled extrusion operators command premium wages, this labor savings is a decisive competitive advantage.
Energy efficiency: One large single-screw extruder (with proportionally larger motor) operates at a higher efficiency point than four small extruders. The barrel heat loss — the dominant thermal inefficiency — is proportional to machine surface area, which is lower for one large extruder than four small ones.
The 4-strand die is engineered with identical flow path length and pressure drop for each cavity, ensuring uniform strap dimensions across all four strands — critical when all strands go to the same customer or specification.
配图建议: 4股打包带同时从模头挤出并穿过拉伸段 (to be acquired)
PET’s most critical processing requirement is not temperature or pressure — it is moisture. PET is hygroscopic: it absorbs 0.3-0.5% moisture from ambient air within hours. When PET containing this moisture is heated to extrusion temperature (260-280°C), the water molecules attack the ester linkages in the polymer backbone through a chemical reaction called hydrolysis. The result:
– Intrinsic viscosity (IV) drops from the feedstock value (typically 0.70-0.80 dL/g for bottle-grade PET) to 0.60 dL/g or below
– Tensile strength of the finished strap drops proportionally — a 0.10 dL/g IV loss can reduce strap strength by 15-25%
– Melt strength drops, causing strap breakage during the hot-stretching operation
– Visible defects appear — surface bubbles, internal voids, silver streaks — that cause strap rejection
Jwell integrates a two-stage drying system upstream of the extruder:
Stage 1 — Crystallization (for amorphous PET bottle flakes): Amorphous PET flakes soften and stick together at 70-80°C in the dryer hopper, forming a solid mass that blocks material flow. The crystallizer heats the flakes to 140-160°C under agitation, inducing crystallization before they enter the main dryer. Crystallized flakes do not stick together at dryer temperature.
Stage 2 — Dehumidifying drying: A desiccant dryer with honeycomb rotor achieves -40°C dew point in the drying air. PET flakes are held at 160-170°C for 4-6 hours, reducing moisture content to below 50 ppm — the industry-standard threshold for high-quality PET strap extrusion. A heated, insulated conveying system between dryer and extruder hopper prevents moisture re-absorption.
For customers running virgin PET resin (pre-crystallized as supplied), only Stage 2 drying is required. For the more common case of recycled bottle flakes, both stages are essential.
配图建议: 除湿干燥系统 + 结晶器 (to be acquired)
The extruded PET strip — as it exits the water bath cooling tank — has the random-coil molecular structure of amorphous PET with tensile strength of only 40-60 MPa. To achieve the 300-800 kg per strap tensile strength that competes with steel strapping, the strip must be hot-stretched — heated to a temperature between the glass transition (approximately 75°C for PET) and the cold crystallization temperature (approximately 130°C), then drawn to 4-7 times its original length.
This hot-stretching process transforms the molecular structure through three simultaneous mechanisms:
Molecular orientation: The polymer chains, mobile at the stretching temperature, align along the strap axis under the drawing tension. This alignment converts the isotropic (equal in all directions) mechanical properties into anisotropic properties — high strength and stiffness along the strap axis, where it is needed.
Strain-induced crystallization: Chain alignment brings PET molecules close enough to crystallize — forming oriented crystallites that act as physical crosslinks, locking in the orientation and preventing molecular relaxation. The degree of crystallinity increases from near-zero (amorphous quenched strip) to 25-40% (oriented strap), depending on stretch ratio and temperature.
Density increase: Oriented and crystallized PET has higher density (approximately 1.37-1.39 g/cm³ versus 1.33 g/cm³ for amorphous PET), reflecting the tighter molecular packing.
The Jwell stretching oven uses multi-zone hot-air circulation with independent zone temperature controllers. The stretch ratio is set through the speed differential between the first and second haul-off — both driven by ABB inverter-controlled motors — and displayed on the Siemens HMI. Typical stretch ratios: 4:1 for general-purpose PET strap, 5:1-6:1 for high-tensile grades, up to 7:1 for maximum-strength applications.
配图建议: 热拉伸烘箱内部或拉伸段 (to be acquired)
Recycled PET bottle flakes present four extrusion challenges that virgin PET resin does not:
Residual moisture: Even after drying, recycled flakes may contain trace moisture in the core of thick flake particles. The extruder’s vented barrel design (atmospheric vent in the decompression zone) provides a secondary moisture removal safeguard.
Variable IV (intrinsic viscosity): Recycled PET from mixed bottle sources has variable IV (0.70-0.80 dL/g range). The extruder must deliver consistent melt quality despite feedstock variability.
Abrasive contaminants: Paper labels, aluminum caps, and dirt not fully removed in the washing process are abrasive. The screw and barrel require wear-resistant metallurgy.
Low bulk density: Washed, dried PET flakes have bulk density of 0.30-0.40 g/cm³ — requiring a larger-diameter feed section for adequate intake.
Jwell’s PET strapping extruder addresses all four challenges:
– 30:1 L/D ratio: Longer than the standard 28:1 for PP, providing the additional residence time needed for complete melting and homogenization of variable-IV recycled feedstock
– Vented barrel: Atmospheric vent removes residual moisture as a safeguard
– Bi-metallic screw and barrel (optional upgrade): CPM-10V or equivalent wear-resistant alloy for extended service life on recycled feedstock
– Large-diameter feed section: Proportionally sized to handle low-bulk-density flake feeding
– Hydraulic double-station screen changer: Filter mesh change without line stoppage — a critical uptime feature for 24/7 recycled-PET production
配图建议: 单螺杆挤出机特写 (to be acquired)
| Parameter | Specification |
| Product | PET (polyethylene terephthalate) strapping band / plastic-steel strap |
| Standard Configuration | 4-strand simultaneous (一出四) |
| Output Range | 300 – 500 kg/h total (4 strands combined) |
| Daily Output | 2 – 12 tons (configuration and strap dimension dependent) |
| Parameter | Specification |
| Extruder Type | Single-screw, vented barrel |
| L/D Ratio | 30:1 |
| Compression Ratio | Application-specific for PET |
| Screw Material | 38CrMoAlA nitrided steel, bi-metallic optional for abrasive feedstock |
| Barrel Material | Bimetallic alloy liner, wear-resistant |
| Heating Zones | Multi-zone, ceramic band heaters, PID control |
| Drive Motor | AC motor with hard-tooth helical gearbox |
| Inverter | ABB or equivalent, variable frequency |
| Screen Changer | Hydraulic double-station, no-line-stop filter change |
| Parameter | Specification |
| Dryer Type | Desiccant, honeycomb rotor |
| Dew Point | -40°C |
| Drying Temperature | 160 – 170°C |
| Residence Time | 4 – 6 hours |
| Target Moisture | < 50 ppm |
| Crystallizer | Included (for amorphous bottle flake feedstock) |
| Material Conveying | Heated, insulated (prevents moisture re-absorption) |
| Parameter | Specification |
| Strap Width | 9 – 32 mm |
| Strap Thickness | 0.5 – 1.5 mm |
| Width Tolerance | ±0.1 mm |
| Thickness Tolerance | ±0.02 mm |
| Tensile Strength | 300 – 800 kg per strap (dimension dependent) |
| Raw Material | Recycled PET bottle flakes (post-consumer) or virgin PET resin |
| Parameter | Specification |
| Material Feeding | Vacuum autoloader or screw feeder |
| Die | Custom T-die, 4-cavity, hard-chrome polished runners |
| Cooling | Stainless steel water tank, chilled water 15-25°C |
| First Haul-off | Dual rubber roller, variable frequency speed control |
| Stretching Method | Hot-air circulation oven, multi-zone temperature control |
| Stretching Temperature | 100 – 180°C (zone-dependent) |
| Stretch Ratio | 4:1 to 7:1 |
| Second Haul-off | Variable frequency speed control |
| Embossing | Pneumatic embossing roller, interchangeable patterns (net, straight, custom) |
| Length Counter | 4 independent digital counters, ±0.5% accuracy, automatic cut-off |
| Winding | 4 independent dual-station automatic coil winders |
| Tension Control | Magnetic-particle brake (standard) / servo (premium) |
| Coil Dimensions | 200-500 mm OD (configurable) |
| Parameter | Specification |
| Line Speed | 80 – 200 m/min per strap |
| Total Installed Power | 120 – 250 kW (configuration dependent) |
| Control System | Siemens PLC + HMI touchscreen |
| Compressed Air | 0.5-0.7 MPa, ≥ 1.0 m³/min |
| Cooling Water | 0.2-0.4 MPa, 15-25°C (requires chiller), flow rate model-dependent |
| Factory Space | ≥ 30 m × 6 m × 5 m height (including dryer, crystallizer area) |
| Parameter | Specification |
| Certifications | CE, ISO 9001 |
| Available as | Complete turnkey solution |
| After-Sales | Global engineer certification, 48-hour spare parts dispatch |
| Warranty | 12 months from acceptance date (wear parts excluded) |
| Property | PET Strap / Steel Strap / PP Strap |
| Tensile Strength | 300-800 kg/strap / 400-1,000 kg/strap / 80-300 kg/strap |
| Weight | ~2.5 g/m (19mm×1.0mm) / ~15 g/m (19mm×0.6mm) / ~2.0 g/m (19mm×0.8mm) |
| Rust/Corrosion | None / Rusts in humidity / None |
| Sharp Edges | None / Sharp — worker injury risk / None |
| Tension Retention | Excellent (85-90% after 4 weeks) / Poor (relaxes under thermal cycling) / Moderate (60-70% after 4 weeks) |
| Elastic Recovery | High — absorbs shock / Near zero — snaps under shock / Moderate |
| Elongation at Break | 10-15% / 5-8% / 15-25% |
| Machine Compatibility | Automatic + semi-automatic only / Manual + pneumatic tools / Automatic + semi-automatic + manual |
| Feedstock | Recycled PET bottle flakes / Virgin steel / Virgin or recycled PP |
| Recyclability | 100% recyclable / Recyclable (scrap metal) / Recyclable |
| Cost per Meter | Medium / Medium-High / Low |
| Best For | Steel replacement, heavy industry, export / Maximum strength, specific machinery / Cartons, pallets, light-medium duty |
| 卡片 | 产品名称 / 链接 / 关系 |
| 1 | PP Strapping Band Extrusion Line / /strapping-extrusion/pp-strapping-band-extrusion-line/ / 打包带系列 — 不同材料 |
| 2 | PET Sheet Extrusion Line / /sheet-extrusion/pet-sheet-extrusion-line/ / 相同材料平台 |
| 3 | rPET Sheet Extrusion Line / /sheet-extrusion/rpet-sheet-extrusion-line/ / 再生PET加工 |
| # | 字段 / 类型 / 必填 / 说明 |
| 1 | Name / text / ✅ / placeholder: “Your full name” |
| 2 | Email / email / ✅ / placeholder: “your@company.com” |
| 3 | Country / select / ✅ / 200+国家 |
| 4 | Phone / tel / — / 含国际区号 |
| 5 | Company / text / — / placeholder: “Your company name” |
| 6 | Application / select / ✅ / Steel Industry / Lumber & Building Materials / Export Crating / Cotton & Textile / Multiple / Other |
| 7 | Feedstock Type / select / ✅ / Recycled PET Bottle Flakes / Virgin PET Resin / Both / Not sure |
| 8 | Number of Strands / select / ✅ / 4-strand (standard) / Other (please specify) |
| 9 | Strap Width Range (mm) / select / ✅ / 9-19 / 19-25 / 25-32 / Full range |
| 10 | Target Output (kg/h) / select / ✅ / <300 / 300-500 / >500 / Not sure |
| 11 | Project Timeline / select / — / Immediate / 1-3 months / 3-6 months / 6-12 months / Information only |
| 12 | Message / textarea / — / placeholder: “Tell us about your production requirements…” |
| — | CAPTCHA / — / ✅ / reCAPTCHA v3 |
| — | Submit / submit / — / “Request Quote & Configuration” |
| # | 检查项 / 状态 |
| 1 | 唯一 H1,含完整产品名 + 核心关键词 / ✅ |
| 2 | H2 技术关键词覆盖: 4-strand, recycled PET, dehumidifying, stretch ratio, steel replacement / ✅ |
| 3 | 规格表为 HTML <table> 文本 / ✅ |
| 4 | 所有图片有描述性 alt 属性 / ✅ |
| 5 | 面包屑用 Schema BreadcrumbList / ✅ |
| 6 | FAQ 用 Schema FAQPage (5个Q&A) / ✅ |
| 7 | 产品信息用 Schema Product + 详细 Organization / ✅ |
| 8 | Canonical 自引用 / ✅ |
| 9 | Title tag 50-60 chars / ✅ |
| 10 | Meta description 含核心关键词 (recycled PET, steel replacement, 4-strand) / ✅ |
| 11 | Open Graph 完整 / ✅ |
| 信号 | 体现方式 |
| Experience | 7步工艺详解(结晶→干燥→挤出→冷却→拉伸→压花→收卷)、4股一出四配置、软PET水解机理 |
| Expertise | PET 水解化学原理、分子取向拉伸、IV/水分<50ppm规范、拉伸比4:1-7:1、30:1 L/D设计 |
| Authoritativeness | 29年经验、8大基地、3500+员工、25000+设备、1000+专利、CE+ISO 9001 |
| Trustworthiness | 全球工程师认证体系、48小时备件调度、12个月保修、120+国家 |
| 检查项 | 目标值 |
| LCP | < 2.5s |
| CLS | < 0.1 |
| INP | < 200ms |
| Mobile-friendly | ✅ |
| 图片格式 | WebP (建议) |
| 资源类型 | 文件夹 / 状态 |
| 主图 (Hero images) | 主图/ / ❌ 目录不存在 |
| 详情图 (Application images) | 详情图/ / ❌ 目录不存在 |
| 视频 (Product videos) | 视频/ / ❌ 目录不存在 |
| 案例照片 (Case study) | Case Study/ / ❌ 目录不存在 |
| PPT/PDF (参考资料) | — / ❌ 目录不存在 |
| 用途 | 资源类型 / 优先级 |
| [C] Hero 画廊 — 产线主图 | 2-3张产品照片 / 高 |
| [C] Hero 画廊 — 工艺段特写 | 1-2张工艺照片 / 高 |
| [D] FAT 视频 — 4股完整生产演示 | 视频 (.mp4) / 高 |
| [D] 生产现场视频 — 各工位特写 | 视频 (.mp4) / 中 |
| [F1] 4股打包带同时挤出 | 照片 / 高 |
| [F2] 除湿干燥系统 + 结晶器 | 照片 / 高 |
| [F3] 热拉伸烘箱/拉伸段 | 照片 / 高 |
| [F4] 单螺杆挤出机特写 | 照片 / 中 |
| [F5] 压花辊近景 + 压花后表面 | 照片 / 中 |
| [F6] 4工位自动收卷机 | 照片 / 高 |
| [F7] HMI 操作界面 / 电控柜 | 照片 / 低 |
| [H1] 钢铁行业应用 — PET带捆扎钢卷 | 照片/示意图 / 高 |
| [H2] 木材建材应用 — PET带捆扎木材 | 照片/示意图 / 高 |
| [H3] 出口包装应用 — PET带捆扎出口箱 | 照片/示意图 / 高 |
| [H4] 棉花打包应用 — PET带捆扎棉包 | 照片/示意图 / 中 |
| 视频封面图 ×2 | 缩略图 / 高 |
| 相关产品卡片缩略图 | 3张 / 中 |
| 客户 logo 条 | 品牌logo集 / 低 |
| Case Study 案例素材 | 照片 + 视频 / 中 |
| 产品手册/目录 | PDF / 中 |
| 目标页面 | 位置 / 锚文本 |
| PP Strapping Band Line | [K] Related Products / “PP Strapping Band Extrusion Line” |
| PET Sheet Line | [K] Related Products / “PET Sheet Extrusion Line” |
| rPET Sheet Line | [K] Related Products / “rPET Sheet Extrusion Line” |
| 来源页面 | 链接上下文 |
| Strapping Extrusion Pillar Page | 打包带挤出分类页 |
| Heavy Industry Packaging Solutions | 重工业包装方案页 |
| PET Recycling & Processing | PET 回收加工整体方案页 |
| Export Packaging Equipment | 出口包装设备页 |
| 维度 | ABS 线 / PET Strapping 线 |
| 挤出机类型 | 单螺杆 33:1 L/D (排气式) / 单螺杆 30:1 L/D (排气式) |
| 产品形态 | 片材 (0.5-6.0 mm) / 打包带 (9-32 mm 宽) |
| 核心工艺 | 挤出→三辊压光→牵引→收卷 / 结晶→干燥→挤出→水浴→拉伸→压花→4工位收卷 |
| 物料处理 | 干燥(ABS除湿) / 结晶 + 除湿干燥(PET <50ppm) |
| Hero 卖点数 | 9 项 / 8 项 |
| 标签页 | 5 个 (+案例) / 4 个 |
| 功能区块 | 8 个 / 7 个 |
| 视频数 | 2 个 / 0 个 (全部 to be acquired) |
| 应用场景数 | 4 个 / 4 个 |
| 独特区块 | 市场地位 + 案例 / PET vs Steel vs PP 对比 |
| 案例素材 | 6 张照片 + 视频 (印尼海尔) / 无 (全部 to be acquired) |
| E-E-A-T 重心 | 市场地位 + 规模验证 / 技术深度 (PET化学 + 水解 + 取向) |
| 特色数据 | 300+冰箱线/90%份额/海尔20年 / 4股一出四/450kg/h/钢带替代/再生PET |
配图: (to be acquired)
The steel and metal industry was the earliest and remains the largest adopter of PET strapping as a steel strap replacement. PET strap bundles steel coils (hot-rolled, cold-rolled, galvanized), steel pipes, metal profiles, aluminum ingots, and copper cathodes — applications where steel strapping was the historical standard but where PET now dominates for four reasons:
Rust elimination: Steel strap rusts during outdoor coil storage, causing rust staining that damages the top layer of expensive finished steel products — a defect that steel mills deduct from the coil price. PET strap is completely rust-proof.
Worker safety: Steel strap cut with hand tools creates razor-sharp edges that cause the most common injury in steel coil warehouses. PET strap has no sharp edges and is cut with standard scissors.
Weight reduction: PET strap at 1/6 the weight of steel reduces shipping weight (and freight cost) and eliminates the disposal cost of used steel strapping.
Tension retention: PET strap’s elasticity allows it to absorb the thermal expansion and contraction of steel coils during temperature changes, maintaining bundle integrity where rigid steel strap would loosen.
The 25-32 mm wide PET strap sizes — standard specifications for steel coil bundling — are produced on the Jwell 4-strand line at 300-500 kg/h.
配图: (to be acquired)
Lumber mills, engineered wood product manufacturers, brick and tile producers, and building materials distributors use PET strap to bundle products that are stored outdoors for months before delivery to construction sites. Key requirements:
Outdoor durability: PET strap with UV stabilizer (added as masterbatch at the extruder) retains tensile strength and color during 6-12 months of outdoor exposure. This is essential for lumber bundles stored in open yards.
High strength: 25-32 mm wide PET strap delivers 500-800 kg tensile strength to secure heavy lumber bundles, brick packs (1-2 tons), and ceramic tile pallets through long-distance transport.
No staining: Unlike steel strap (rust) and some PP strap formulations (plasticizer migration), PET strap does not leave marks or stains on the wood surface — important for appearance-grade lumber.
Recyclable: Used PET strap from the construction site is collected and recycled, closing the material loop from bottle flake feedstock to strap to recycled flake for new strap.
PET strapping band — often called plastic-steel strap — delivers comparable tensile strength (300-800 kg per strap) to steel strapping at approximately 1/6 the weight. Beyond the weight advantage, PET strap is completely rust-proof (eliminating rust stains on finished goods), has no sharp edges (eliminating worker injuries from cut steel band), retains tension better during long transport cycles due to elasticity, and is 100% recyclable. For steel mills, lumber mills, brick manufacturers, and export craters, the total cost of ownership calculation — accounting for material cost, worker safety, product damage from rust, and disposal — increasingly favors PET over steel.
The 4-strand configuration extrudes four PET straps simultaneously from a single T-die, each traveling through the stretching oven and wound on its own independent winding station. This configuration delivers approximately 450 kg/h total output from one extruder, one control system, and one operator — maximizing per-ton capital, labor, and energy efficiency. The standard PET strap market demands high volume (steel mills, cotton gins consuming tons of strap per day), and the 4-strand line meets that demand at the lowest per-ton cost.
PET strapping is primarily produced from recycled post-consumer PET bottle flakes — washed, sorted by color, and processed into clean flake. The recycled feedstock reduces raw material cost by 30-50% versus virgin PET resin and supports circular-economy procurement. Virgin PET resin is also usable for premium applications requiring maximum optical clarity or the most consistent tensile strength. The feedstock must pass through a crystallizer (for amorphous bottle flakes) and dehumidifying dryer to achieve <50 ppm moisture before extrusion.
PET is hygroscopic — it absorbs moisture from air. Without drying, the moisture in PET flakes (typically 0.3-0.5%) causes hydrolysis during extrusion at 260-280°C: water molecules break the ester linkages in the PET polymer chain, reducing molecular weight (intrinsic viscosity drops from 0.70-0.80 dL/g to below 0.60), reducing tensile strength by 15-25%, reducing melt strength (causing strap breakage during stretching), and producing visible bubbles/streaks on the strap surface. Jwell’s integrated dryer system reduces moisture to <50 ppm, the industry-standard target for defect-free PET strap.
Three factors determine PET strap tensile strength: (1) Feedstock IV — higher intrinsic viscosity PET produces stronger strap (bottle-grade 0.70-0.80 dL/g is standard); (2) Stretch ratio — higher draw ratios (4:1 to 7:1) produce higher molecular orientation and therefore higher strength, up to the practical limit where further stretching causes strand breakage; (3) Strap dimensions — wider and thicker straps have proportionally higher absolute tensile strength. The Jwell line’s independent haul-off speed control and multi-zone stretching oven allow the operator to dial in the exact stretch ratio for the target strength specification.
Jwell WPC Flooring Production Line produces lightweight, durable wood-plastic composite flooring with a foamed core, precision calendering, embossing, UV coating and automated profiling.
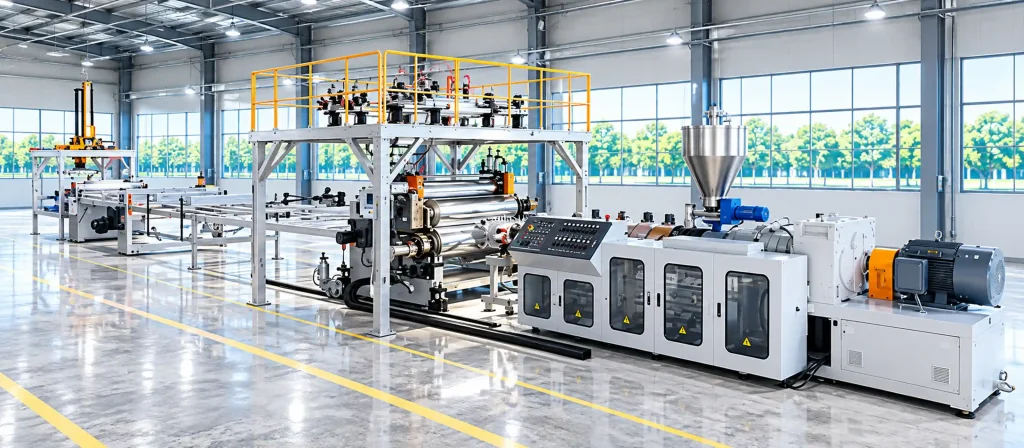
Jwell SPC Flooring Production Line delivers turnkey production from mixing and extrusion to calendering, UV coating, profiling, lamination and packaging.
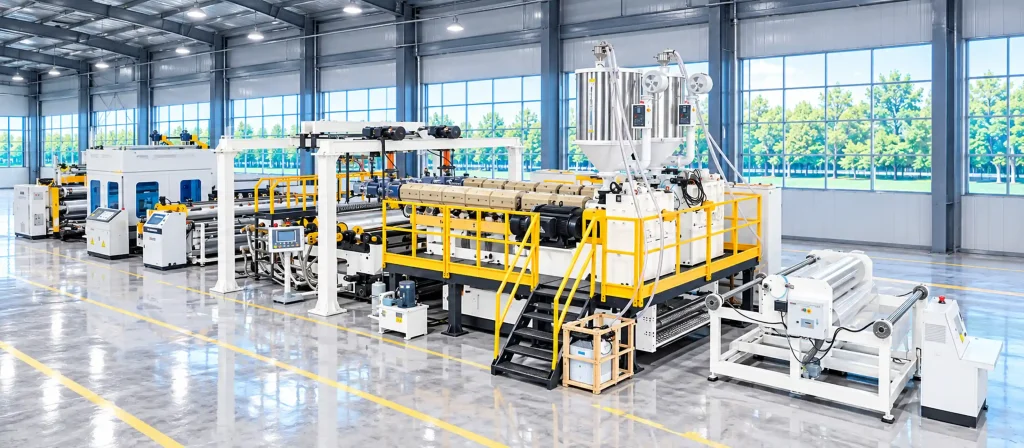
JWELL TPU Casting & Laminating Film Extrusion Line integrates precision casting, online lamination and automatic winding to produce TPU composite films and laminated fabrics for footwear, textiles and outdoor applications.
Jwell Machinery Co., Ltd sets up in 1997 , we are large manufacturer of plastic extrusion machinery in China, our headoffice was located in Shanghai.
SOLUTIONS
PRODUCTS
CONTACT
Copyright © Jwell Machinery Co., Ltd 2026. All rights reserved. Privacy Policy | Terms & Conditions | Site Map
Tell us about your specific requirements. Our team can help you identify a solution for your project.