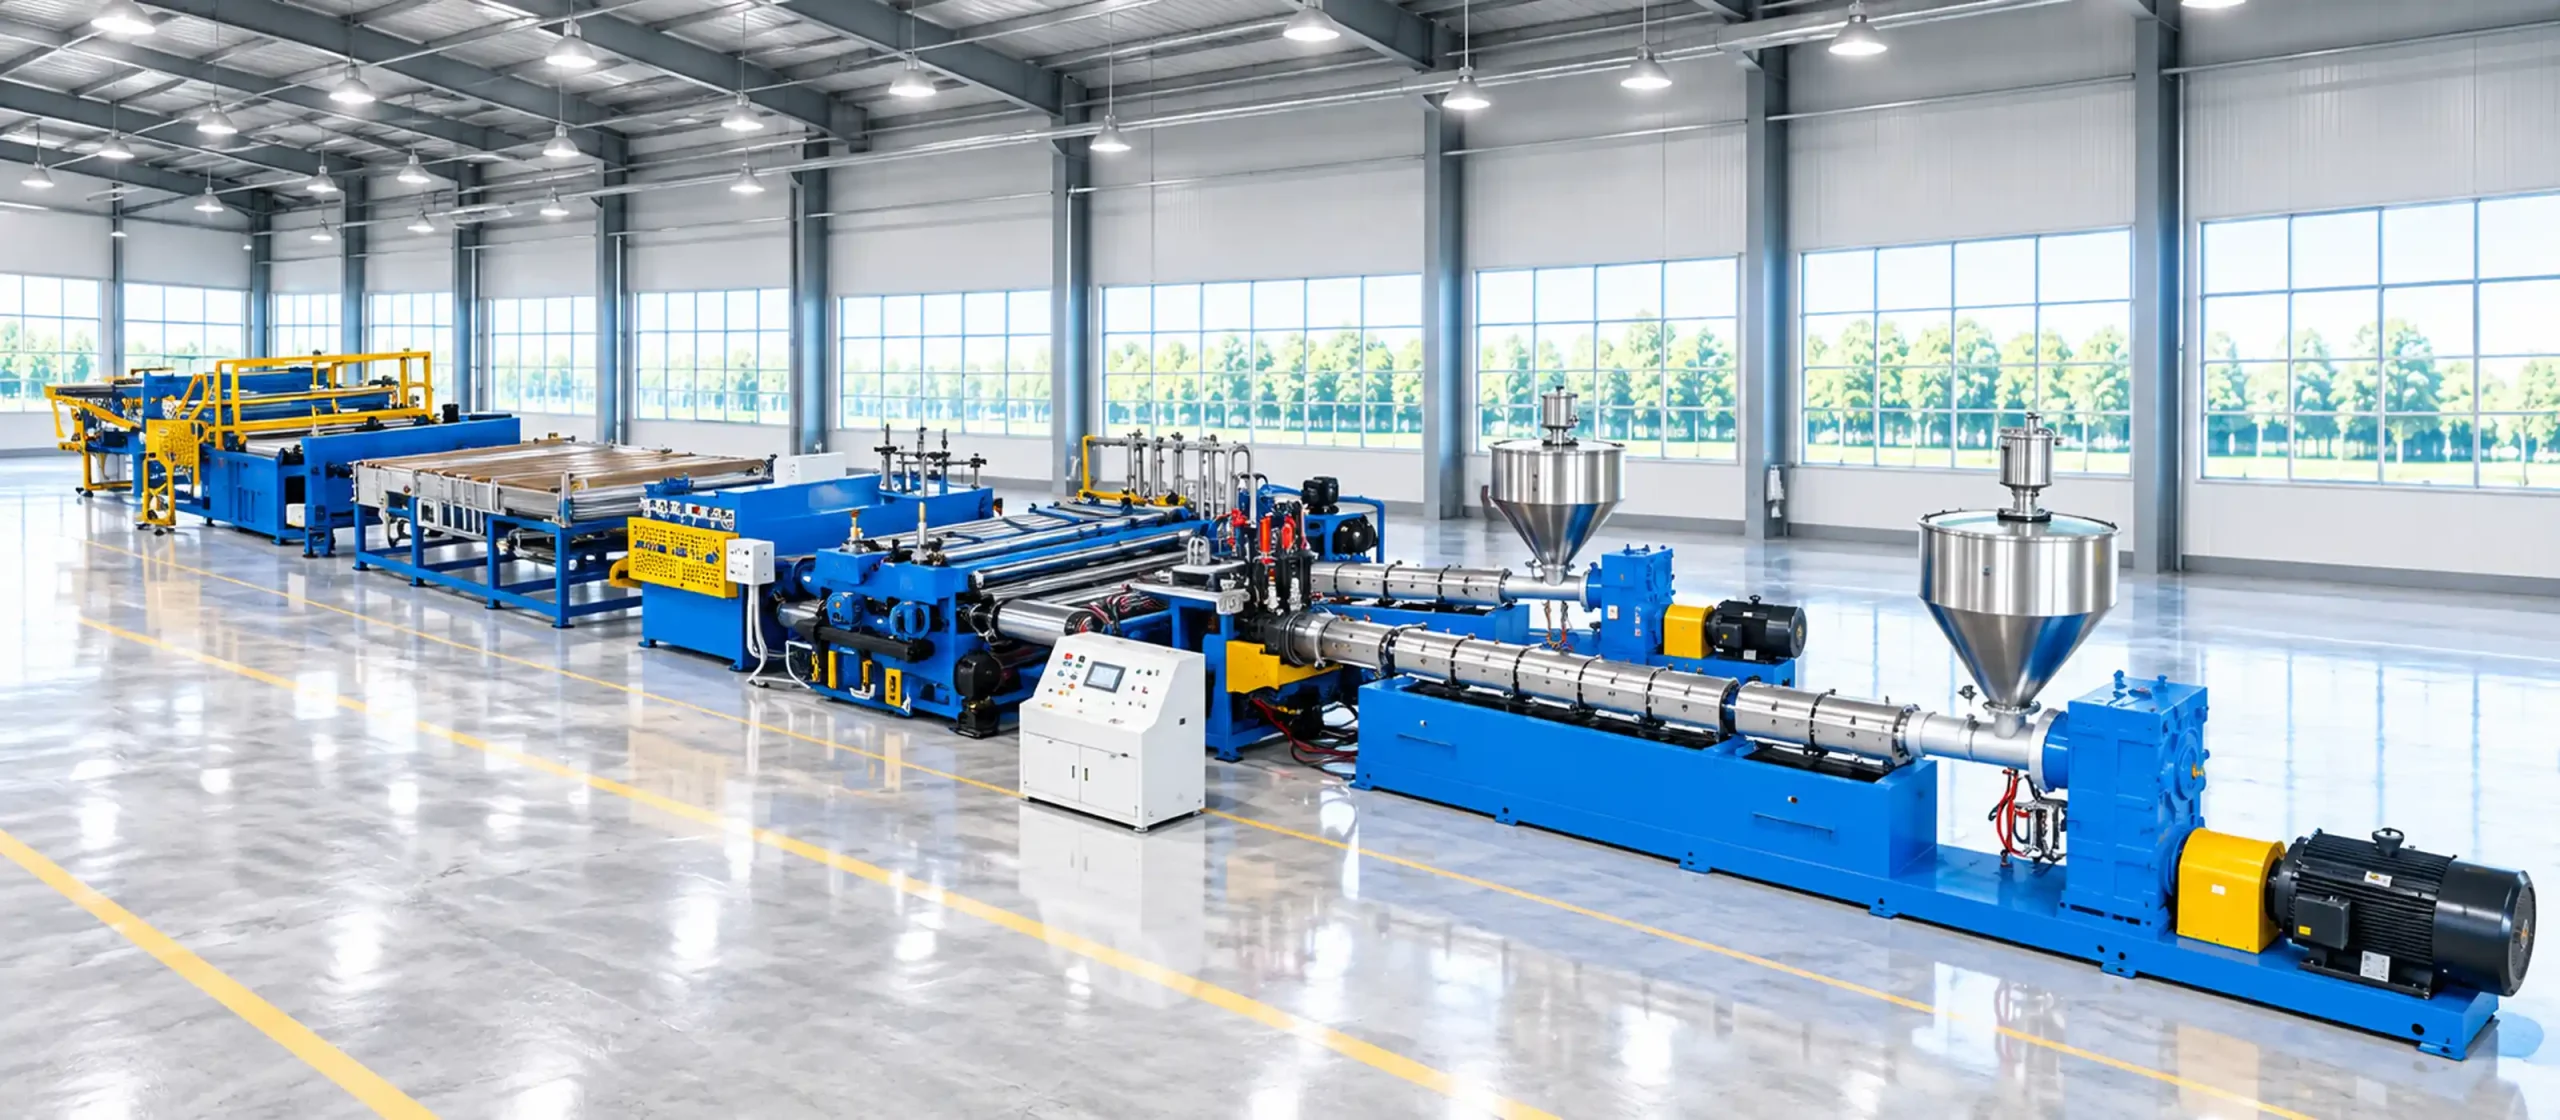
WPC Flooring Production Line
Jwell WPC Flooring Production Line produces lightweight, durable wood-plastic composite flooring with a foamed core, precision calendering, embossing, UV coating and automated profiling.
The PP Hollow Plate Extrusion Line is part of JWELL’s complete extrusion portfolio. Customers evaluating this PP Hollow Plate Extrusion Line also frequently request our PP Hollow Sheet Line | Jwell Machinery and PP Thick Plate Extrusion Line | 3-30mm | 500-800kg/h | Jwell Machinery, which share the same proven screw, die and control platforms. For layout drawings, pricing and lead times, contact JWELL Machinery directly.
| # | Item | Key Point |
| 1 | 🌀 Parallel Twin-Screw Extruder | Processes 50-100% Recycled PP with CaCO3 Filler — SEO: parallel twin screw extruder PP, recycled PP extrusion, PP hollow sheet extruder, twin screw sheet extrus |
| 2 | ⚡ Twin-Wall Sheet Die + Vacuum Calibration | Consistent Flute Structure, Uniform Wall Thickness — SEO: twin wall sheet die, PP hollow plate die, vacuum calibration sheet, corrugated plastic die |
| 3 | The defining s | |
| 4 | 🎯 Inline Fabrication Options | Produce Finished Boxes and Sign Boards Directly from the Extrusion Line — SEO: inline punching hollow plate, inline slitting corrugated plastic, PP box production line, hollow plate fa |
| 5 | 🔄 Multi-Component Gravimetric Dosing | Regrind, Virgin, Filler, Color, UV — All in One Blend — SEO: gravimetric dosing PP hollow plate, calcium carbonate filler dosing, recycled PP formulation, multi-compo |
PP hollow plate production economics depend on feedstock cost, not resin cost. Standard hollow plate formulations use 50-100% post-industrial or post-consumer recycled PP, with 10-30% calcium carbonate filler by weight. This feedstock presents three processing challenges that make single-screw extruders unsuitable: (1) recycled PP flake has variable bulk density (0.3-0.55 g/cm³) causing feed instability and output surging in single-screw gravity-fed hoppers, (2) CaCO3 filler is abrasive and accelerates screw/barrel wear in single-screw friction-dependent conveying, and (3) the combination of regrind, filler, and color masterbatch requires compounding-level mixing that single-screw designs cannot provide.
Jwell’s parallel twin-screw extruder addresses all three. The intermeshing, co-rotating screws provide positive displacement conveying — each screw flight transports a defined volume of material forward regardless of bulk density, eliminating the surging that causes thickness variation. The screw elements are modular: conveying elements move the material forward, kneading blocks disperse the filler and homogenize the blend, and mixing elements distribute the color masterbatch uniformly. This compounding capability means the extruder accepts PP regrind flake, CaCO3 powder, and color masterbatch pellets directly — no pre-compounding step required.
Screw diameter options: 75 mm, 92 mm, or 110 mm depending on target output. The 38CrMoAlA nitrided screw elements (HV≥740, 0.5-0.7 mm nitrided layer) provide 3-5 year service life processing standard CaCO3-filled formulations. For high-filler applications (>20% CaCO3), Jwell offers bimetallic barrel liners (58-62 HRC) and CPM-10V screw elements that extend service life to 5-7 years.
—
SEO: twin wall sheet die, PP hollow plate die, vacuum calibration sheet, corrugated plastic die
The defining structural feature of PP hollow plate is its flute geometry — vertical ribs spaced at 3-8 mm intervals connecting two flat surface layers. This structure creates bending stiffness from geometry (the ribs act as I-beam webs between the surface flanges), not from material thickness, achieving a stiffness-to-weight ratio approximately 5-8 times higher than solid PP sheet of equal weight.
Jwell’s twin-wall die is a specialized flat die with internal mandrels that form the hollow flutes. The die is designed with separate melt flow channels for the top surface, bottom surface, and vertical ribs, with independent flow adjustment for each channel. The die lips are chrome-plated (Ra 0.05 μm) with adjustable flexible-lip design for sheet thickness control.
Immediately after the die, the vacuum calibration tank applies controlled vacuum (typically -0.02 to -0.05 MPa) to the still-molten sheet surface, drawing it against polished calibration plates that fix the flute geometry and surface finish while the PP crystallizes. This vacuum calibration is the critical process step that determines final product quality — insufficient vacuum results in collapsed flutes and inconsistent wall thickness; excessive vacuum causes surface marking from the calibration plates. The Jwell system uses multi-zone vacuum control with independent regulation for top and bottom surfaces, enabling asymmetric calibration for applications requiring different surface finishes on each side (e.g., smooth for printing on one side, textured for slip resistance on the other).
—
SEO: inline punching hollow plate, inline slitting corrugated plastic, PP box production line, hollow plate fabrication
PP hollow plate’s market value increases dramatically when delivered as finished products rather than raw sheet. A 4 mm PP hollow sheet sells for approximately $1.50-2.00/m²; a finished reusable box made from that same sheet sells for $4.00-6.00/m² equivalent. Jwell’s inline fabrication options enable customers to capture this value-add within the production line, eliminating offline fabrication labor and work-in-process inventory.
Available inline modules:
– Cross-Cutter: Pneumatic or servo-driven guillotine cutter, cut-to-length accuracy ±1 mm, speed synchronized with line speed
– Hole Punching: Pneumatic punch press with interchangeable die sets — produces grommet holes (for signage), handle cutouts (for box blanks), and ventilation holes (for agricultural trays)
– Longitudinal Slitting: Rotary slitting blades with adjustable spacing — produces multiple narrow strips from full-width sheet for edge protection profiles
– Creasing & Folding: Heated creasing bars (140-160°C) that locally compress the flute structure to create fold lines, followed by mechanical folding stations — produces box blanks ready for assembly
– Automatic Stacking: Pneumatic stacker with programmable sheet count (10-100 sheets per stack), automatic stack ejection conveyor
The fabrication modules operate in sequence, controlled by the Siemens PLC, with automatic product-length tracking to maintain registration between cutting, punching, and creasing positions — critical for box blank production where handle position, fold line position, and overall blank dimensions must align within ±2 mm.
—
SEO: gravimetric dosing PP hollow plate, calcium carbonate filler dosing, recycled PP formulation, multi-component blending extrusion
PP hollow plate formulations are cost-optimized recipes that vary by application. A signage-grade formulation might use 70% recycled PP, 20% CaCO3, 7% virgin PP, 2% color masterbatch, and 1% UV stabilizer. A food-grade packaging formulation uses 100% virgin PP with food-contact colorants. A construction formwork formulation uses 60% regrind, 30% CaCO3, 8% virgin PP, and 2% carbon black. Each formulation represents a different cost structure and market segment, and the ability to switch between them without hardware changes determines a manufacturer’s market flexibility.
Jwell’s multi-component gravimetric dosing system meters up to six components by weight: PP regrind (from grinder), virgin PP pellets, CaCO3 powder (from silo), color masterbatch, UV stabilizer, and processing aid. Each component has an independent weigh hopper with load cell (±0.5% batch accuracy) and loss-in-weight monitoring. The blender PLC calculates the batch composition from percentage setpoints entered at the HMI, dispenses each component sequentially into the mixing chamber, blends for a programmed cycle time, and discharges to the extruder feed hopper.
The system’s gravimetric (by weight) rather than volumetric operation is essential for CaCO3 filler — calcium carbonate has a bulk density of 0.8-1.2 g/cm³ (varies by particle size and compaction) compared to PP pellets at 0.5-0.6 g/cm³, making volumetric metering inaccurate by ±5-8% in filler content. This variation directly affects sheet stiffness and cost — a 5% excess of CaCO3 above specification adds material cost while degrading impact strength.
—
| Parameter | JW-HP75 / JW-HP92 / JW-HP110 |
| Extruder | / / |
| Extruder Type | Parallel co-rotating twin screw / Parallel co-rotating twin screw / Parallel co-rotating twin screw |
| Screw Diameter | 75 mm / 92 mm / 110 mm |
| L/D Ratio | 36:1 / 36:1 / 36:1 |
| Screw Material | 38CrMoAlA, nitrided HV≥740 / 38CrMoAlA, nitrided HV≥740 / 38CrMoAlA, nitrided HV≥740 |
| Barrel Liner | Bimetallic 58-62 HRC (optional) / Bimetallic 58-62 HRC (optional) / Bimetallic 58-62 HRC (optional) |
| Main Motor Power | 110 kW / 160 kW / 220 kW |
| Output Capacity | 200-350 kg/h / 350-500 kg/h / 450-600 kg/h |
| Die & Calibration | / / |
| Die Type | Twin-wall flat die, chrome-plated / Twin-wall flat die, chrome-plated / Twin-wall flat die, chrome-plated |
| Die Width | up to 1600 mm / up to 2100 mm / up to 2500 mm |
| Calibration Type | Multi-zone vacuum, dual-surface / Multi-zone vacuum, dual-surface / Multi-zone vacuum, dual-surface |
| Vacuum Range | -0.02 to -0.06 MPa / -0.02 to -0.06 MPa / -0.02 to -0.06 MPa |
| Product Range | / / |
| Sheet Thickness | 2-8 mm / 2-10 mm / 2-12 mm |
| Sheet Width | 600-1500 mm / 800-2000 mm / 1000-2500 mm |
| Flute Spacing | 3-8 mm (interchangeable) / 3-8 mm (interchangeable) / 3-8 mm (interchangeable) |
| Flute Wall Uniformity | ±0.1 mm / ±0.1 mm / ±0.1 mm |
| Surface Finish | Smooth / Matte / Textured / Smooth / Matte / Textured / Smooth / Matte / Textured |
| Color Options | Natural, White, Black, Red, Blue, Green, Yellow, Custom / / |
| Fabrication (Optional) | / / |
| Cross-Cutter Accuracy | ±1 mm / ±1 mm / ±1 mm |
| Hole Punching | Interchangeable die sets / Interchangeable die sets / Interchangeable die sets |
| Slitting | Adjustable, up to 5 strips / Adjustable, up to 7 strips / Adjustable, up to 9 strips |
| Stacker | Pneumatic, 10-100 sheets/stack / Pneumatic, 10-100 sheets/stack / Pneumatic, 10-100 sheets/stack |
| Dosing System | / / |
| Components | Up to 6 (regrind, virgin, CaCO3, color, UV, additive) / / |
| Batch Accuracy | ±0.5% / ±0.5% / ±0.5% |
| Control & Utilities | / / |
| PLC | Siemens S7-1200 / Siemens S7-1200 / Siemens S7-1200 |
| HMI | 12″ touchscreen / 12″ touchscreen / 12″ touchscreen |
| Main Motor Brand | WEG / WEG / WEG |
| Inverter | ABB ACS880 / ABB ACS880 / ABB ACS880 |
| Total Installed Power | ~200 kW / ~300 kW / ~400 kW |
| Line Dimensions (L×W×H) | 25×4×3.5 m / 30×5×3.5 m / 35×6×4 m |
| Certifications | CE, ISO 9001 / CE, ISO 9001 / CE, ISO 9001 |
PP hollow plate’s defining market advantage is replacing single-use corrugated cardboard in industrial logistics. A standard cardboard box survives 1-3 trips through a supply chain before crushing, tearing, or water damage renders it unusable. A PP hollow plate box of equivalent dimensions survives 20-50 trips, is washable (industrial parts washers, pressure wash), waterproof, and chemically resistant to oils, greases, and mild acids common in manufacturing environments.
This reusability transforms the packaging cost equation. A cardboard box costing $2.00 that lasts 3 trips has a per-trip cost of $0.67. A PP hollow plate box costing $8.00 that lasts 40 trips has a per-trip cost of $0.20 — a 70% cost reduction over the box’s service life. Automotive tier-1 suppliers, electronics manufacturers, and food processing plants have adopted PP hollow plate returnable packaging systems for inter-plant and supplier-to-OEM logistics, achieving documented packaging cost reductions of 50-80%.
Jwell’s hollow plate line supports the full reusable packaging ecosystem: sheet in 3-6 mm thickness for boxes, dividers, and dunnage; die-cut blanks (with inline punching) for specific part nests; and color coding for part-number or production-line identification. The ability to run 50-100% recycled PP feedstock aligns the packaging with corporate sustainability targets for circular economy and waste reduction.
—
PP hollow plate is the standard material for temporary outdoor signage worldwide — election campaign signs, real estate “For Sale” boards, construction site signage, event directional signs, and retail point-of-purchase displays. The material’s combination of outdoor durability (UV-stabilized grades maintain color and mechanical properties for 2-5 years), printability (screen printing, UV digital printing, vinyl film lamination), lightweight handling (a 1200×800 mm sign board weighs approximately 0.8-1.2 kg), and low cost ($1.50-3.00/m² for substrate) has made it the dominant signage substrate for temporary outdoor applications.
Jwell lines serving the signage market typically run white sheet in 3-5 mm thickness at widths of 1200-1600 mm (standard sign board dimensions). UV-stabilized formulations with 1-2% HALS (hindered amine light stabilizer) and UV absorber provide the 2-5 year outdoor service life that sign printers require. The inline cutting and stacking system delivers sheet ready for direct printing, eliminating offline cutting labor.
—
PP hollow plate (also called corrugated plastic board, twin-wall sheet, or Correx/Coroplast) is a lightweight structured sheet made from polypropylene with hollow flutes between two flat surfaces. It combines the strength-to-weight ratio of corrugated cardboard with the water resistance and durability of plastic. Primary applications include reusable packaging boxes, signage and display boards, concrete construction formwork, greenhouse panels, protective packaging sheets, and automotive component dividers. It is 100% recyclable and widely used as a sustainable replacement for single-use cardboard and wood packaging.
The Jwell line produces PP hollow plate from 2 mm to 12 mm thickness with width up to 2500 mm. Common production thicknesses: 2-3 mm for packaging and signage, 4-6 mm for reusable boxes and construction formwork, 8-12 mm for heavy-duty industrial packaging and structural panels. The vacuum calibration system maintains uniform flute geometry and wall thickness across the full sheet width.
PP hollow plate production typically uses a high percentage of recycled PP (50-100%) and calcium carbonate filler (10-30%), creating a feedstock with variable bulk density, inconsistent melt flow, and abrasive mineral content. A parallel twin-screw extruder handles these challenges that would cause surging and screw wear in a single-screw machine. The twin-screw’s positive conveying mechanism is independent of barrel friction, so it processes low-bulk-density regrind flake and high-filler compounds without output fluctuation. The intermeshing screws also provide compounding action that homogenizes PP regrind with filler and color masterbatch in a single step, eliminating the need for pre-compounding.
Yes. The gravimetric dosing system meters PP regrind, virgin PP, calcium carbonate, color masterbatch, and UV stabilizer in any ratio specified by the product application. Color changeover between production campaigns is accomplished through recipe selection on the Siemens PLC — extruder temperature profile, screw RPM, and vacuum calibration parameters are all stored per product recipe. The line processes standard PP homopolymer, PP copolymer (for low-temperature impact applications), UV-stabilized PP (for outdoor signage), anti-static PP (for electronics packaging), and flame-retardant PP (V-2 or V-0 rated for construction).
The standard Jwell line includes inline cross-cutting (pneumatic or servo-driven guillotine cutter, cut-to-length accuracy ±1 mm), and automatic stacking (pneumatic stacker with preset sheet count). Optional inline equipment includes: inline hole punching (for signage grommet holes and box handle cutouts), longitudinal slitting (for producing narrower strip widths from full-width sheet), edge folding/creasing (for box blank production), and automatic strapping/palletizing. These options enable the line to deliver finished, ready-to-use products — packaging boxes, sign boards, or formwork panels — directly from the extrusion line without offline fabrication steps.
Jwell WPC Flooring Production Line produces lightweight, durable wood-plastic composite flooring with a foamed core, precision calendering, embossing, UV coating and automated profiling.
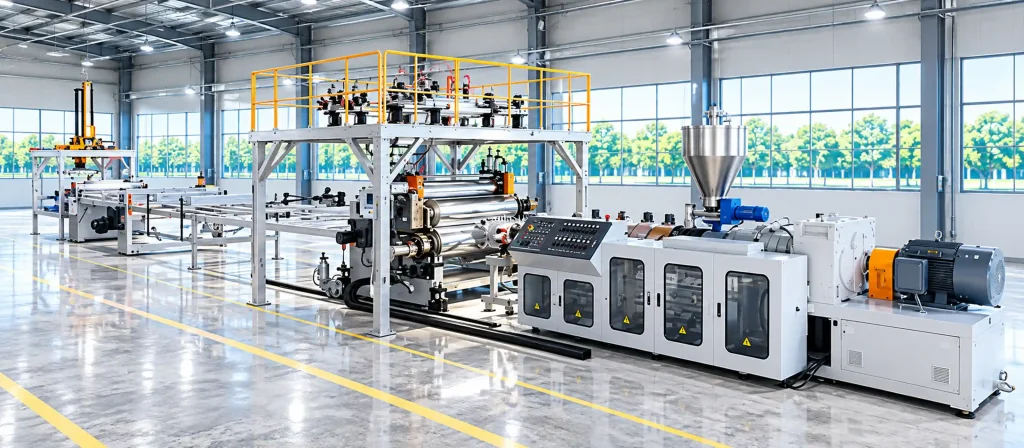
Jwell SPC Flooring Production Line delivers turnkey production from mixing and extrusion to calendering, UV coating, profiling, lamination and packaging.
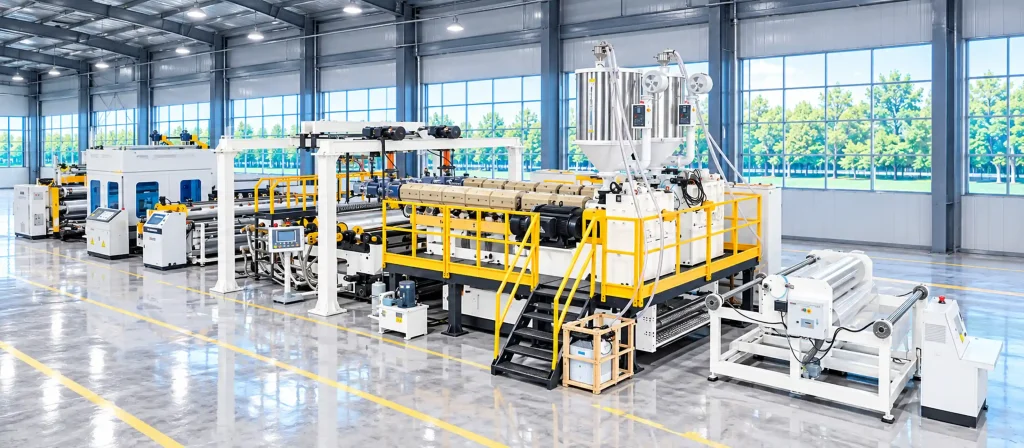
JWELL TPU Casting & Laminating Film Extrusion Line integrates precision casting, online lamination and automatic winding to produce TPU composite films and laminated fabrics for footwear, textiles and outdoor applications.
Jwell Machinery Co., Ltd sets up in 1997 , we are large manufacturer of plastic extrusion machinery in China, our headoffice was located in Shanghai.
SOLUTIONS
PRODUCTS
CONTACT
Copyright © Jwell Machinery Co., Ltd 2026. All rights reserved. Privacy Policy | Terms & Conditions | Site Map
Tell us about your specific requirements. Our team can help you identify a solution for your project.