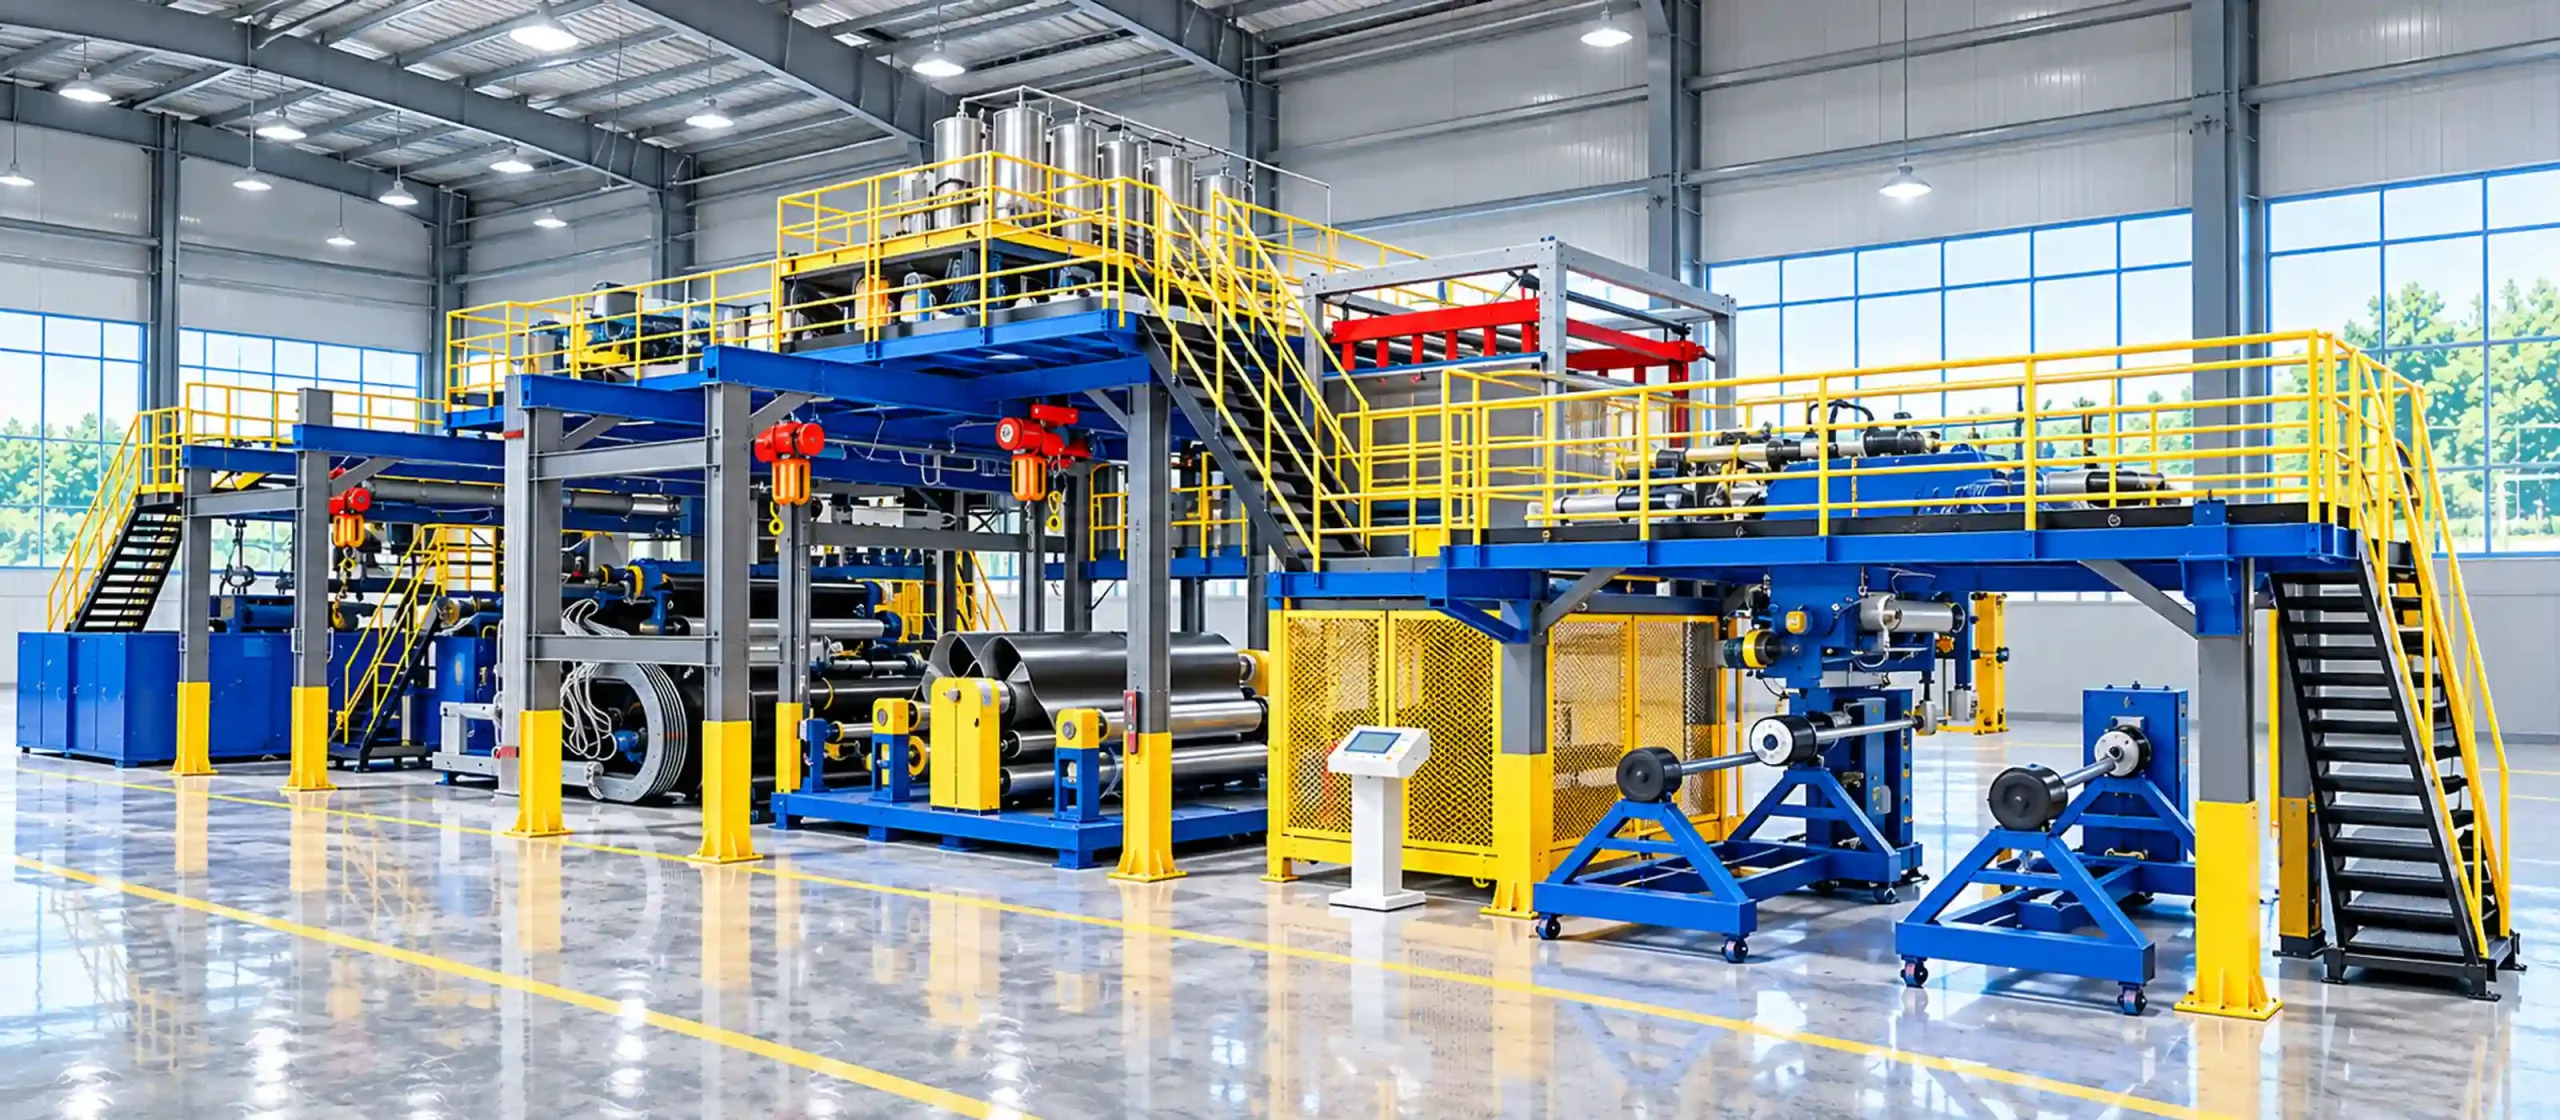
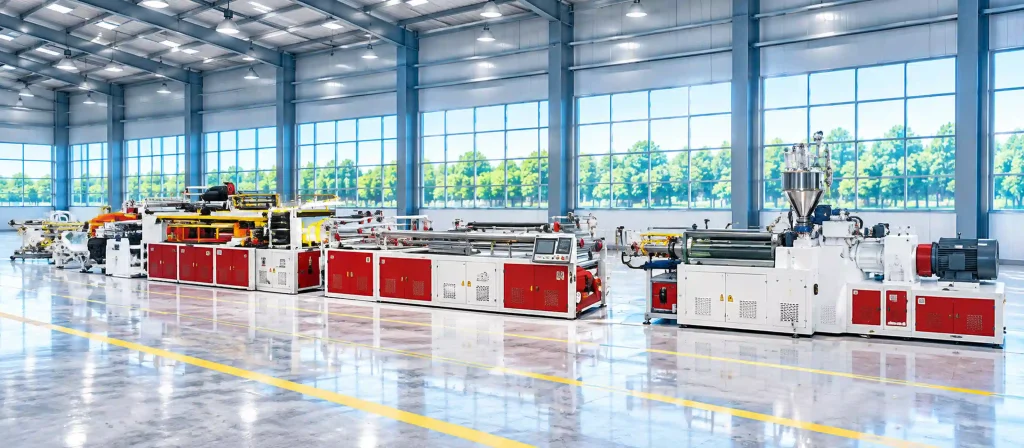
WPC Flooring Production Line
Jwell WPC Flooring Production Line produces lightweight, durable wood-plastic composite flooring with a foamed core, precision calendering, embossing, UV coating and automated profiling.
The HDPE Geomembrane Line is part of JWELL’s complete extrusion portfolio. Customers evaluating this HDPE Geomembrane Line also frequently request our TPO Waterproof Membrane Line | Jwell Machinery and PVC Waterproof Membrane Line | Jwell Machinery, which share the same proven screw, die and control platforms. For layout drawings, pricing and lead times, contact JWELL Machinery directly.
The Jwell HDPE geomembrane extrusion line achieves sheet widths up to 8,000mm (8 meters) in a single pass — one of the widest single-pass geomembrane production capabilities available in the global market. This ultra-wide capability is enabled by the proprietary waterproof sheet T-die design with CAD-optimized manifold geometry, paired with a high-precision three-roll calendar that maintains uniform sheet profile across the full width.
For landfill liner and reservoir lining projects, the field installation advantage is substantial. An 8-meter wide geomembrane panel covers 40-60% more area per panel compared to the 4-5 meter panels typical of narrower production lines. This directly translates to:
– 60% reduction in field seam welding — fewer seams mean lower installation labor costs and reduced welding equipment time
– Reduced leakage risk — every seam is a potential leak path; fewer seams directly improve containment system integrity
– Faster installation — larger panels cover more ground per shift, accelerating project timelines
– Lower QA/QC cost — seam testing (destructive and non-destructive) scales linearly with seam count
The 8-meter width has been validated in production installations including the Kazakhstan 7-meter project, where Jwell’s equipment produces wide-width geomembrane for environmental containment applications under demanding Central Asian climate conditions.
配图: 8-meter-waterproof-membrane.webp — 8米宽幅防水板生产主图
The extrusion system is built around three precision components that determine sheet quality and production stability:
Nordson Melt Pump (USA): Positioned between the extruder and the screen changer, the Nordson melt pump stabilizes melt pressure and flow rate, eliminating the pressure fluctuations inherent to single-screw extrusion. This ensures consistent sheet thickness across the full web width and length, reduces thickness tolerance to within ±0.05mm, and enables lower scrap rates during production start-up and steady-state operation. The melt pump decouples the melting and pumping functions, allowing the extruder to focus on plasticization while the gear pump delivers a constant, surge-free flow to the die.
38CrMoAlA Screw & Barrel: The screw and barrel are manufactured from 38CrMoAlA nitrided steel — a premium grade specifically engineered for plastic extrusion applications. The nitrided surface layer of 0.5-0.7mm provides exceptional wear resistance, with screw surface hardness of HV≥740 and barrel surface hardness of HV≥940. Under normal operating conditions with virgin HDPE resin, the screw and barrel deliver 5-7 years of service life. The screw geometry is optimized for HDPE geomembrane grade resins (MI 0.05-0.15 g/10min), delivering consistent melt homogeneity at output rates up to 1,000 kg/h.
Hydraulic Screen Changer (Double Column Double Position): The double-column, double-position hydraulic screen changer enables continuous filtration without production interruption. When one filter screen becomes clogged, the hydraulic system shifts to the second position, allowing the dirty screen to be replaced while production continues. This design eliminates the 15-30 minute downtime associated with single-position screen changers, maximizing production uptime for 24-hour continuous operation.
配图: hdpe-geomembrane-extrusion-line-hero-02.webp — 主机及熔体泵特写
The T-die is the single most critical component for achieving uniform geomembrane thickness across wide sheet widths. Jwell’s waterproof sheet T-die incorporates five advanced design features:
1. CAD-Optimized Manifold: The die manifold is designed using computational fluid dynamics (CFD) simulation to optimize melt flow distribution across the full die width. The manifold geometry ensures that melt velocity and pressure are uniform from center to edge, eliminating the thickness variations that plague dies designed by trial-and-error methods.
2. Lengthening Die Lip: The extended die lip provides a longer flow path for the polymer melt, allowing residual stress to relax before the sheet exits the die. This produces a flatter, lower-stress sheet with reduced post-extrusion shrinkage — critical for geomembrane dimensional stability during field installation.
3. Micro-Adjustable Upper Die Lip: The upper die lip features precision adjustment mechanisms (individual thermal bolts or mechanical adjusters) that enable operators to fine-tune the die gap at each position across the width. When integrated with the online thickness gauge feedback, this enables real-time closed-loop thickness control.
4. Changeable Lower Die Lip: The lower die lip is designed as a replaceable insert, allowing rapid changeover between different thickness ranges (1-4mm standard production, up to 10mm maximum capability). This enables a single die to serve multiple product specifications without purchasing a second die.
5. Restrictor Bar Adjustment: An adjustable restrictor bar upstream of the die lip provides coarse flow distribution tuning, enabling optimization for different resin grades and output rates without re-machining the die.
The T-die supports a standard thickness range of 1.0-4.0mm for geomembrane production, with maximum capability of 10mm for specialized applications. Surface finish and chroming ensure HDPE release without sticking or surface defects.
配图建议: T-die 结构示意图,标注五大设计特征
The three-roll calendar is the heart of the sheet forming and cooling process. Jwell’s roller calendar system is engineered to geomembrane-grade precision standards that directly impact sheet flatness, surface quality, and thickness uniformity:
Material & Manufacturing: The rollers are forged from 42CrMo alloy steel — a grade commonly specified for heavy-duty mechanical components requiring high strength and toughness. Each roller undergoes precision machining to achieve the following specifications:
Hydraulic Gap Adjustment: The roll gap between the top and middle rollers is adjusted via a hydraulic system, enabling precise, repeatable gap setting across the full roller face. This hydraulic adjustment provides:
– Continuous gap control — operators can fine-tune sheet thickness without stopping production
– Uniform pressure distribution — hydraulic cylinders apply equal force across the roller width, preventing edge-to-center thickness variation
– Recipe-driven positioning — the PLC stores gap positions for each product recipe, enabling one-touch changeover between thickness specifications
Temperature Control: Each roller is individually temperature-controlled via a closed-loop pressurized water circuit, maintaining temperature uniformity of ±1°C across the full face width. This eliminates the thermal expansion variations that cause localized thickness bands — a defect visible as periodic striping in geomembrane sheet.
For textured geomembrane production, the middle roller accepts interchangeable patterned sleeves that create the surface roughness required for slope stability in landfill and reservoir applications.
配图: hdpe-geomembrane-extrusion-line-hero-03.webp — 三辊压光及冷却段
| Parameter | Specification |
| Available Configurations | Standard geomembrane line (400-600 kg/h) / High-output line (600-1,000 kg/h) |
| Extruder Model | JW-150 single-screw (150mm) / JW-180 single-screw (180mm) |
| Alternative Configuration | JW-150/160 parallel twin-screw or JW-200 single-screw (optional) |
| Output Range (configuration dependent) | 400 – 1,000 kg/h |
| Parameter | Specification |
| Extruder Type | Single-screw (standard for HDPE geomembrane) |
| Screw Diameter | 150 mm / 180 mm |
| Screw Material | 38CrMoAlA nitrided steel |
| Nitrided Layer | 0.5 – 0.7 mm |
| Screw Surface Hardness | HV ≥ 740 |
| Barrel Surface Hardness | HV ≥ 940 |
| Barrel Heating Zones | Multi-zone, independent PID control |
| Heating Type | Cast aluminum heaters with PID temperature control |
| Drive Motor | WEG / ABB high-efficiency AC motor |
| Inverter | ABB series |
| Parameter | Specification |
| Melt Pump | Nordson (USA) — stabilizes melt pressure and flow rate |
| Screen Changer Type | Hydraulic, double column double position |
| Screen Changer Operation | Continuous (no production stoppage for screen change) |
| Filter Mesh | Customizable per resin and quality requirements |
| Parameter | Specification |
| Die Type | Waterproof sheet T-die (flat die) |
| Manifold Design | CAD-optimized with CFD flow simulation |
| Die Lip Feature | Lengthening die lip for stress relaxation |
| Upper Die Lip | Micro-adjustable (thermal bolts or mechanical) |
| Lower Die Lip | Changeable insert for multi-thickness production |
| Restrictor Bar | Adjustable for flow distribution optimization |
| Standard Thickness Range | 1.0 – 4.0 mm |
| Maximum Thickness Capability | 10 mm |
| Die Width | Matched to target sheet width (up to 8,000mm) |
| Parameter | Specification |
| Configuration | Three-roll vertical calendar |
| Roll Material | 42CrMo forged steel |
| Roll Diameter | Application-specific (typically 400-600 mm) |
| Coaxiality | ≤ 0.005 mm |
| Surface Roughness | Ra ≤ 0.016 μm (mirror finish) |
| Surface Hardness | HRC 58 – 62 |
| Chrome Plating | 0.08 mm |
| Gap Adjustment | Hydraulic, continuous, recipe-driven |
| Temperature Control | Individual closed-loop per roll, ±1°C uniformity |
| Surface Options | Smooth (standard) / Interchangeable textured sleeves for roughened geomembrane |
| Parameter | Specification |
| Sheet Width | 2,000 – 8,000 mm |
| Sheet Thickness | 1.0 – 3.0 mm (standard) / up to 4.0 mm (extended) |
| Thickness Tolerance | ±0.05 mm (with closed-loop die adjustment) |
| Surface Type | Smooth / Single-side textured / Double-side textured |
| Textured Surface Friction Angle | 27 – 33 degrees (GRI-GM13 compliant) |
| Raw Material | HDPE virgin resin (MI 0.05-0.15 g/10min, density 0.935-0.945 g/cm³) |
| Carbon Black Content | 2.0 – 3.0% (UV resistance) |
| Parameter | Specification |
| Thickness Gauge | Scanning frame type O (continuous full-width measurement) |
| Thickness Feedback | Closed-loop to T-die micro-adjustable upper die lip |
| Laser Printing | CO2 laser — product ID, date, batch number, traceability |
| Edge Trimming | Automatic edge cutters on cooling bracket |
| Parameter | Specification |
| Cooling Bracket | Extended cooling roller section with haul off |
| Edge Cutters | Automatic, synchronized with line speed |
| Haul Off Unit | Constant-tension, synchronized with extruder output |
| Winder | Automatic tension control, roll length counting |
| Max Roll Weight | Several tons (configuration dependent) |
| Parameter | Specification |
| Control System | Siemens PLC with color HMI touch screen |
| Electrical Components | Schneider contactors & relays, ABB inverters |
| Recipe Storage | Multiple product recipes, one-touch changeover |
| Process Parameters Logged | 50+ at 10-second intervals, time-stamped, non-editable |
| Industry 4.0 | Bus communication, MES/ERP integration capability |
| Remote Diagnostics | Via WeChat/WhatsApp, 2-hour response (GMT+8) |
| Parameter | Specification |
| Haul-off Speed | 0.5 – 5.0 m/min |
| Total Installed Power | 350 – 650 kW (configuration dependent) |
| Power Supply | 380V / 50Hz (customizable to 440V/60Hz) |
| Machine Dimensions (L×W×H) | ~45,000 × 6,500 × 4,200 mm (configuration dependent) |
| Parameter | Specification |
| Equipment Certifications | CE, ISO 9001 |
| Product Compliance | GRI-GM13, ASTM D-6384, ASTM D-5397, JIS K 6732 |
| Tunnel Application | CRCC (China Railway Construction Corporation) certified |
| Potable Water | NSF/ANSI 61 (with NSF-approved resin) |
| After-Sales | Global engineer certification system, 48-hour spare parts dispatch, 12-month warranty |
| Parameter | Detail |
| Sheet Width | 7,000 mm (7 meters) |
| Sheet Thickness | 1.5 – 3.0 mm |
| Production Capacity | 600 – 800 kg/h |
| Extruder Configuration | Single-screw JW-180 |
| Target Applications | Landfill liner, mining containment, reservoir lining |
| Commissioning | On-site installation and operator training by Jwell engineers |
| Base | Location / Specialty |
| Shanghai | Shanghai, China / Headquarters & R&D center |
| Suzhou | Jiangsu, China / Sheet & plate extrusion lines |
| Changzhou | Jiangsu, China / Sheet extrusion & precision components |
| Zhejiang | Zhejiang, China / Pipe & profile extrusion |
| Guangdong | Guangdong, China / Southern China production hub |
| Anhui | Anhui, China / Large-scale manufacturing base |
| Thailand | Southeast Asia / International manufacturing & service |
| Germany | Europe / Technology & European market service |
| 卡片 | 产品名称 / 链接 / 关系 |
| 1 | TPO Geomembrane Extrusion Line / /sheet-extrusion/tpo-geomembrane-extrusion-line/ / 同类产品(热塑性聚烯烃防水板) |
| 2 | PE Waterproof Membrane Extrusion Line / /sheet-extrusion/pe-waterproof-membrane-extrusion-line/ / 材料相近(PE基防水卷材) |
| 3 | PP Geogrid Extrusion Line / /sheet-extrusion/pp-geogrid-extrusion-line/ / 应用重叠(岩土工程材料) |
| Component | Material / Nitrided Layer / Surface Hardness |
| Screw | 38CrMoAlA / 0.5 – 0.7 mm / HV ≥ 740 |
| Barrel | 38CrMoAlA / 0.5 – 0.7 mm / HV ≥ 940 |
| Phase | Duration / Description |
| Manufacturing | 60 – 90 days / From order confirmation and down payment to completion of manufacturing |
| Factory Acceptance Test | 3 – 5 days / Customer visit to Jwell’s Changzhou facility to verify line performance with their resin |
| Shipping | 7 – 14 days (Asia) / 25 – 40 days (Europe/Americas/Africa) / Sea freight to destination port |
| Customs clearance | 3 – 7 days / Destination country dependent |
| On-site installation & commissioning | 15 – 30 days / Jwell engineers install, calibrate, and test the line at customer facility |
| Operator training | 5 – 7 days / Hands-on training during commissioning |
| Total | ~4 – 6 months / Order to production start |
| # | 字段 / 类型 / 必填 / 说明 |
| 1 | Name / text / ✅ / placeholder: “Your full name” |
| 2 | Email / email / ✅ / placeholder: “your@company.com” |
| 3 | Country / select / ✅ / 200+国家 |
| 4 | Phone / tel / — / 含国际区号 |
| 5 | Company / text / — / placeholder: “Your company name” |
| 6 | Application / select / ✅ / Landfill / Mining / Tunnel / Reservoir & Canal / Building Waterproofing / Multiple / Other |
| 7 | Target Sheet Width / select / ✅ / 2,000-4,000mm / 4,000-6,000mm / 6,000-7,000mm / 7,000-8,000mm / Not sure |
| 8 | Required Output (kg/h) / select / ✅ / 400-600 / 600-800 / 800-1,000 / >1,000 / Not sure |
| 9 | Sheet Thickness (mm) / select / — / 1.0-2.0 / 2.0-3.0 / 3.0-4.0 / Other |
| 10 | Project Timeline / select / — / Immediate / 1-3 months / 3-6 months / 6-12 months / Information only |
| 11 | Message / textarea / — / placeholder: “Tell us about your production requirements, target resin grade, and project specifications…” |
| — | CAPTCHA / — / ✅ / reCAPTCHA v3 |
| — | Submit / submit / — / “Request Quote & Configuration” |
| 断点 | 宽度 / 适配变化 |
| Desktop | ≥ 1200px / 完整双列布局,Hero 图文左右排列 |
| Tablet | 768 – 1199px / Hero 改为上下堆叠,规格表横向滚动 |
| Mobile | < 768px / 单列布局,标签页改为手风琴折叠,视频全宽 |
| 元素 | 移动端处理 |
| Hero 画廊 | 改为 swipe 滑动画廊,主图 + 缩略图改为水平滑动 |
| 技术规格表 | 大表格改为卡片式纵向排列,每组参数可折叠展开 |
| 标签页 | 横向滚动标签改为纵向手风琴折叠 |
| FAQ | 手风琴交互,默认全部折叠 |
| 询价表单 | 单列纵向排列,select 下拉使用原生组件 |
| 视频 | 全宽 16:9,preload=”metadata” 节省流量 |
| 面包屑 | 折叠为 Home > … > HDPE Geomembrane |
| 检查项 | 目标值 |
| LCP (Largest Contentful Paint) | < 2.5s |
| CLS (Cumulative Layout Shift) | < 0.1 |
| INP (Interaction to Next Paint) | < 200ms |
| 图片格式 | WebP(已满足) |
| 首屏图片 | loading=”eager”(仅主图) |
| 非首屏图片 | loading=”lazy” |
| 视频预加载 | preload=”metadata” 仅加载元数据 |
| 字体 | 系统字体栈,无外部字体加载 |
| 文件夹 | 文件 / 用途 / 状态 |
| 主图/ | 8-meter-waterproof-membrane.webp / [C] Hero 画廊 — 主图 1(8米宽幅生产) / ✅ |
| 主图/ | hdpe-geomembrane-extrusion-line-hero-02.webp / [C] Hero 画廊 — 主机及熔体泵特写 / ✅ |
| 主图/ | hdpe-geomembrane-extrusion-line-hero-03.webp / [C] Hero 画廊 — 三辊压光及冷却段 / ✅ |
| 主图/ | hdpe-geomembrane-extrusion-line-hero-04.webp / [C] Hero 画廊 — 卷取及成品 / ✅ |
| 详情图/ | landfill-liner-systems.webp / [H1] 填埋场应用 / ✅ |
| 详情图/ | mining-and-tailings-containment.webp / [H2] 矿山尾矿应用 / ✅ |
| 详情图/ | tunnel-and-underground-waterproofing.webp / [H3] 隧道地下防水应用 / ✅ |
| 详情图/ | water-reservoir-and-canal-lining.webp / [H4] 水库渠道应用 / ✅ |
| 视频/ | HDPE Geomembrane Line.mp4 / [D1] 产品概览视频 / ✅ |
| 视频/ | 7 meters Geomembrane sheet extrusion line project in Kazakhstan.mp4 / [D2] 哈萨克斯坦案例视频 / ✅ |
| 用途 | 建议 / 优先级 |
| F1 超宽生产能力配图 | 8米宽幅板材现场安装对比照片(宽板 vs 窄板) / 高 |
| F2 Nordson 熔体泵特写 | 熔体泵及液压换网器近景照片 / 中 |
| F3 T-die 结构图 | 防水片材模头剖面图,标注五大设计特征 / 中 |
| F4 辊筒精度配图 | 42CrMo 辊筒近景,展示镜面光洁度及液压间隙调节机构 / 中 |
| F5 自动化配图 | 在线测厚仪扫描架 + CO2 激光打印近景 / 中 |
| 视频封面图 ×2 | 产品视频 + 哈萨克斯坦案例视频 poster 图 / 高 |
| 相关产品卡片图 | TPO 防水板 / PE 防水卷材 / PP 土工格栅 缩略图 / 中 |
| 公司数据可视化 | 8 大生产基地地图 + 25,000+ 安装量数据图 / 低 |
| 客户项目照片 | 哈萨克斯坦项目现场照片(如有) / 中 |
| 螺杆材料特写 | 38CrMoAlA 螺杆表面氮化层特写 / 硬度测试照片 / 低 |
| # | 检查项 / 状态 |
| 1 | 唯一 H1,含完整产品名 + 核心关键词 / ✅ |
| 2 | H2 技术关键词覆盖: geomembrane, HDPE, waterproof sheet, T-die, Nordson melt pump, 38CrMoAlA, 42CrMo roller / ✅ |
| 3 | 规格表为 HTML <table> 文本 / ✅ |
| 4 | 所有图片有描述性 alt 属性 / ✅ |
| 5 | 面包屑用 Schema BreadcrumbList / ✅ |
| 6 | FAQ 用 Schema FAQPage (7个Q&A) / ✅ |
| 7 | 产品信息用 Schema Product + 详细 Organization / ✅ |
| 8 | 视频 ×2 分别用 Schema VideoObject / ✅ |
| 9 | Canonical 自引用 / ✅ |
| 10 | Title tag 50-60 chars / ✅ |
| 11 | Meta description 含技术亮点 + 社会证明数据 / ✅ |
| 12 | Open Graph 完整 / ✅ |
| 信号 | 体现方式 |
| Experience | 29年挤出经验、25,000+ 安装量、哈萨克斯坦7米项目实拍 |
| Expertise | 38CrMoAlA 螺杆/料筒自研、42CrMo 辊筒精密制造、CAD 模头设计、Nordson 熔体泵集成 |
| Authoritativeness | ISO 9001 + CE 认证、1,000+ 专利、8 大全球生产基地、$700M+ 年销售额 |
| Trustworthiness | GRI-GM13 / CRCC / NSF 合规、Siemens PLC + Schneider/ABB 标准化组件、全球200人售后团队 |
| 目标页面 | 位置 / 锚文本 |
| TPO Geomembrane Line | [K] Related Products / “TPO Geomembrane Extrusion Line” |
| PE Waterproof Membrane Line | [K] Related Products / “PE Waterproof Membrane Extrusion Line” |
| PP Geogrid Line | [K] Related Products / “PP Geogrid Extrusion Line” |
| Contact Page | [B] Hero CTA / “Discuss Your Application with an Engineer” |
| 来源页面 | 链接上下文 |
| Sheet Extrusion Pillar Page | 片材挤出分类页 |
| Geomembrane Production Guide | 土工膜生产技术指南 |
| Landfill Liner Materials Comparison | 填埋场防渗材料对比文章 |
| Mining Containment Solutions | 矿山防渗解决方案页 |
| Tunnel Waterproofing Systems Guide | 隧道防水系统指南 |
HDPE geomembrane produced on this line serves as the primary impermeable barrier in municipal solid waste and hazardous waste landfill cells. The wide-width capability (up to 8,000mm) allows installers to cover large base areas with fewer panels, reducing field seam lengths and long-term permeability risk for environmental compliance.
Key requirements for landfill liner geomembrane include:
– Thickness: 1.5-3.0mm per GRI-GM13 standard (2.0mm most common for municipal solid waste)
– Width: 7,000-8,000mm preferred to minimize seam count and installation time
– Surface: Smooth for base liner / Textured for slope liner (friction angle ≥27° for slope stability)
– Carbon black: 2-3% for UV resistance during exposed service before soil cover
– Seam weldability: Consistent thickness and surface for hot-wedge or extrusion welding
Jwell’s geomembrane line produces sheet that meets GRI-GM13 specifications for all physical, mechanical, and endurance properties required by landfill engineering standards worldwide. The scanning thickness gauge ensures every square meter of geomembrane meets the minimum thickness requirement — critical for regulatory compliance where undershoot areas constitute reject material.
Applications within landfill systems: Base liner, side slope liner, leachate collection system liner, final cap/closure liner, and leachate evaporation pond liner.
Open-pit and underground mining operations utilize HDPE geomembrane liners for heap leach pads, tailings storage facilities, and process water containment. HDPE’s chemical resistance to acidic and alkaline leach solutions (pH 2-12), combined with its high tensile strength and puncture resistance, makes it the industry standard for mining containment applications.
The extrusion line’s ability to produce both smooth and textured geomembrane variants suits the demanding mechanical stresses of mining environments:
– Heap leach pads: Textured geomembrane on slopes prevents ore stack slippage; smooth geomembrane on the base facilitates solution collection
– Tailings storage facilities: 2.0-3.0mm HDPE geomembrane provides long-term containment of process water and tailings supernatant
– Process water ponds: Lined with 1.5-2.0mm HDPE geomembrane for recycling of leach solution
– Diversion channels: HDPE-lined channels route clean water away from contaminated areas
The 8-meter wide production capability is particularly valuable for large mining projects where the total liner area may exceed 1 million square meters — wider panels reduce installation time and seam inspection requirements in remote mining locations where labor and equipment mobilization costs are high.
Industry standards: HDPE geomembrane for mining applications typically meets GRI-GM13, with additional project-specific requirements for tensile, puncture, and stress crack resistance validated by ASTM D-6392 (seam peel and shear testing).
The Jwell HDPE geomembrane extrusion line can produce sheets up to 8,000mm (8 meters) wide in a single pass. This ultra-wide capability is achieved through our proprietary waterproof sheet T-die design with CAD manifold and high-precision three-roll calendar. Producing 8-meter wide geomembrane reduces field seam welding by up to 60% compared to narrower production methods — a major cost and quality advantage for landfill and reservoir projects where seam count directly impacts installation labor cost, QA/QC testing cost, and long-term leakage risk.
For applications requiring narrower widths (e.g., tunnel waterproofing at 2,000-4,000mm), the line is configurable with a narrower die and downstream equipment, reducing equipment cost and factory footprint.
Yes, the line produces smooth, single-side textured, and double-side textured HDPE geomembrane. The texturing system uses interchangeable patterned roller sleeves integrated into the three-roll calendar. Surface type changeover requires a roller sleeve swap, which typically takes under 45 minutes with calibrated gap and temperature parameters stored in the PLC for each surface recipe.
Textured geomembrane surfaces achieve a friction angle of 27-33 degrees, meeting GRI-GM13 and ASTM D-6097 specifications for slope stability in landfill and reservoir embankment applications. The texturing does not compromise the sheet’s waterproof integrity or thickness uniformity, as the pattern depth is controlled to within 0.1mm of the nominal sheet thickness.
Jwell HDPE geomembrane extrusion lines are CE certified and manufactured under ISO 9001 quality management systems. The geomembrane produced on our lines has been tested to comply with:
– GRI-GM13: Geosynthetic Research Institute standard for HDPE geomembrane (thickness, tensile, puncture, tear, carbon black content, UV resistance, stress crack resistance)
– ASTM D-6384: Standard terminology for geosynthetics
– ASTM D-5397: Notched constant tensile load (NCTL) test for stress crack resistance
– JIS K 6732: Japanese industrial standard for waterproofing polymer sheets
– CRCC: China Railway Construction Corporation certification for railway tunnel waterproof membranes (including strict requirements for thickness uniformity, tear strength, and surface flatness)
By using NSF-approved HDPE resin, manufacturers can achieve NSF/ANSI 61 certification for potable water contact applications.
The Nordson melt pump, imported from the USA, is positioned between the extruder and the hydraulic screen changer. Its primary functions are:
1. Pressure stabilization: Eliminates the pressure fluctuations (±5-10 bar) inherent to single-screw extrusion, reducing them to ±0.5 bar — a 10:1 improvement that directly translates to sheet thickness uniformity.
2. Flow rate consistency: Delivers a constant, surge-free melt flow to the T-die, eliminating the thickness variations that appear as periodic bands in geomembrane sheet.
3. Throughput optimization: By decoupling the melting and pumping functions, the extruder can focus on plasticization while the gear pump handles pressure development — enabling higher throughput at lower melt temperatures (reducing HDPE thermal degradation risk).
4. Scrap reduction: Stable pressure and flow reduce the start-up scrap period and maintain tighter thickness tolerance during steady-state production, lowering overall scrap rates by 15-30%.
The Nordson brand was selected for its proven reliability in high-output HDPE applications and global availability of replacement parts and service.
The screw and barrel are manufactured from 38CrMoAlA nitrided steel — a premium chromium-molybdenum-aluminum alloy steel specifically engineered for plastic extrusion applications. Key specifications:
The barrel surface is harder than the screw surface (HV 940 vs. HV 740) by design — the barrel is the more expensive component to replace, so the harder surface ensures longer barrel life relative to screw life. The screw is designed as the wear component, expected to be replaced or refurbished at 5-7 year intervals under normal HDPE processing conditions.
For applications involving recycled HDPE material (which may contain contaminants), mineral-filled compounds, or abrasive additives, Jwell offers enhanced wear packages including bimetallic barrel liners (Xaloy X-800 or equivalent, 58-62 HRC) and wear-resistant screw surfaces extending service life by 50-100%.
Jwell WPC Flooring Production Line produces lightweight, durable wood-plastic composite flooring with a foamed core, precision calendering, embossing, UV coating and automated profiling.
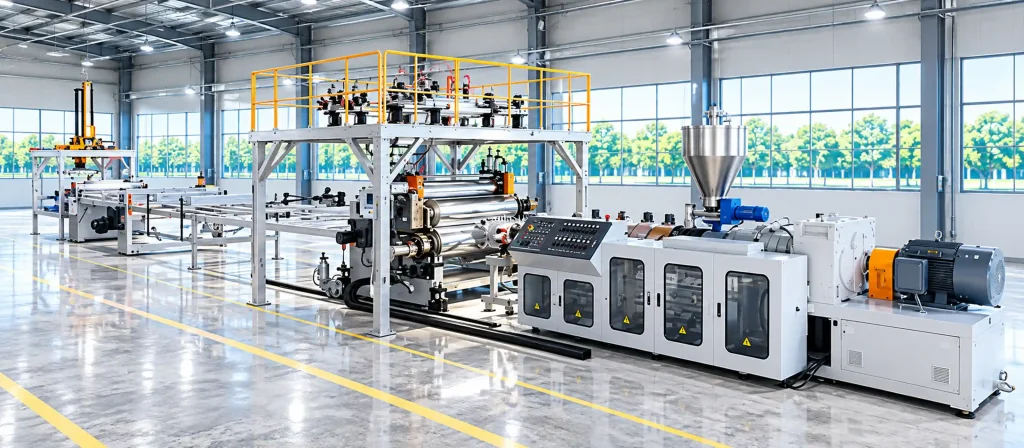
Jwell SPC Flooring Production Line delivers turnkey production from mixing and extrusion to calendering, UV coating, profiling, lamination and packaging.
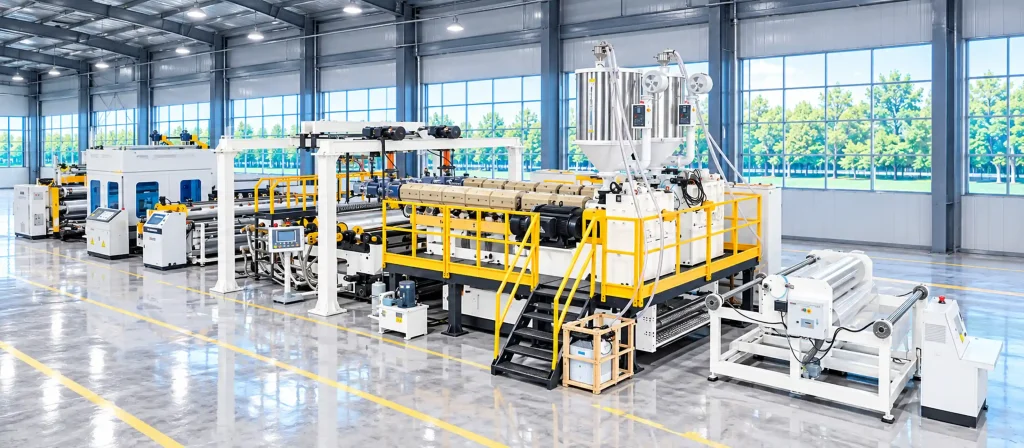
JWELL TPU Casting & Laminating Film Extrusion Line integrates precision casting, online lamination and automatic winding to produce TPU composite films and laminated fabrics for footwear, textiles and outdoor applications.
Jwell Machinery Co., Ltd sets up in 1997 , we are large manufacturer of plastic extrusion machinery in China, our headoffice was located in Shanghai.
SOLUTIONS
PRODUCTS
CONTACT
Copyright © Jwell Machinery Co., Ltd 2026. All rights reserved. Privacy Policy | Terms & Conditions | Site Map
Tell us about your specific requirements. Our team can help you identify a solution for your project.