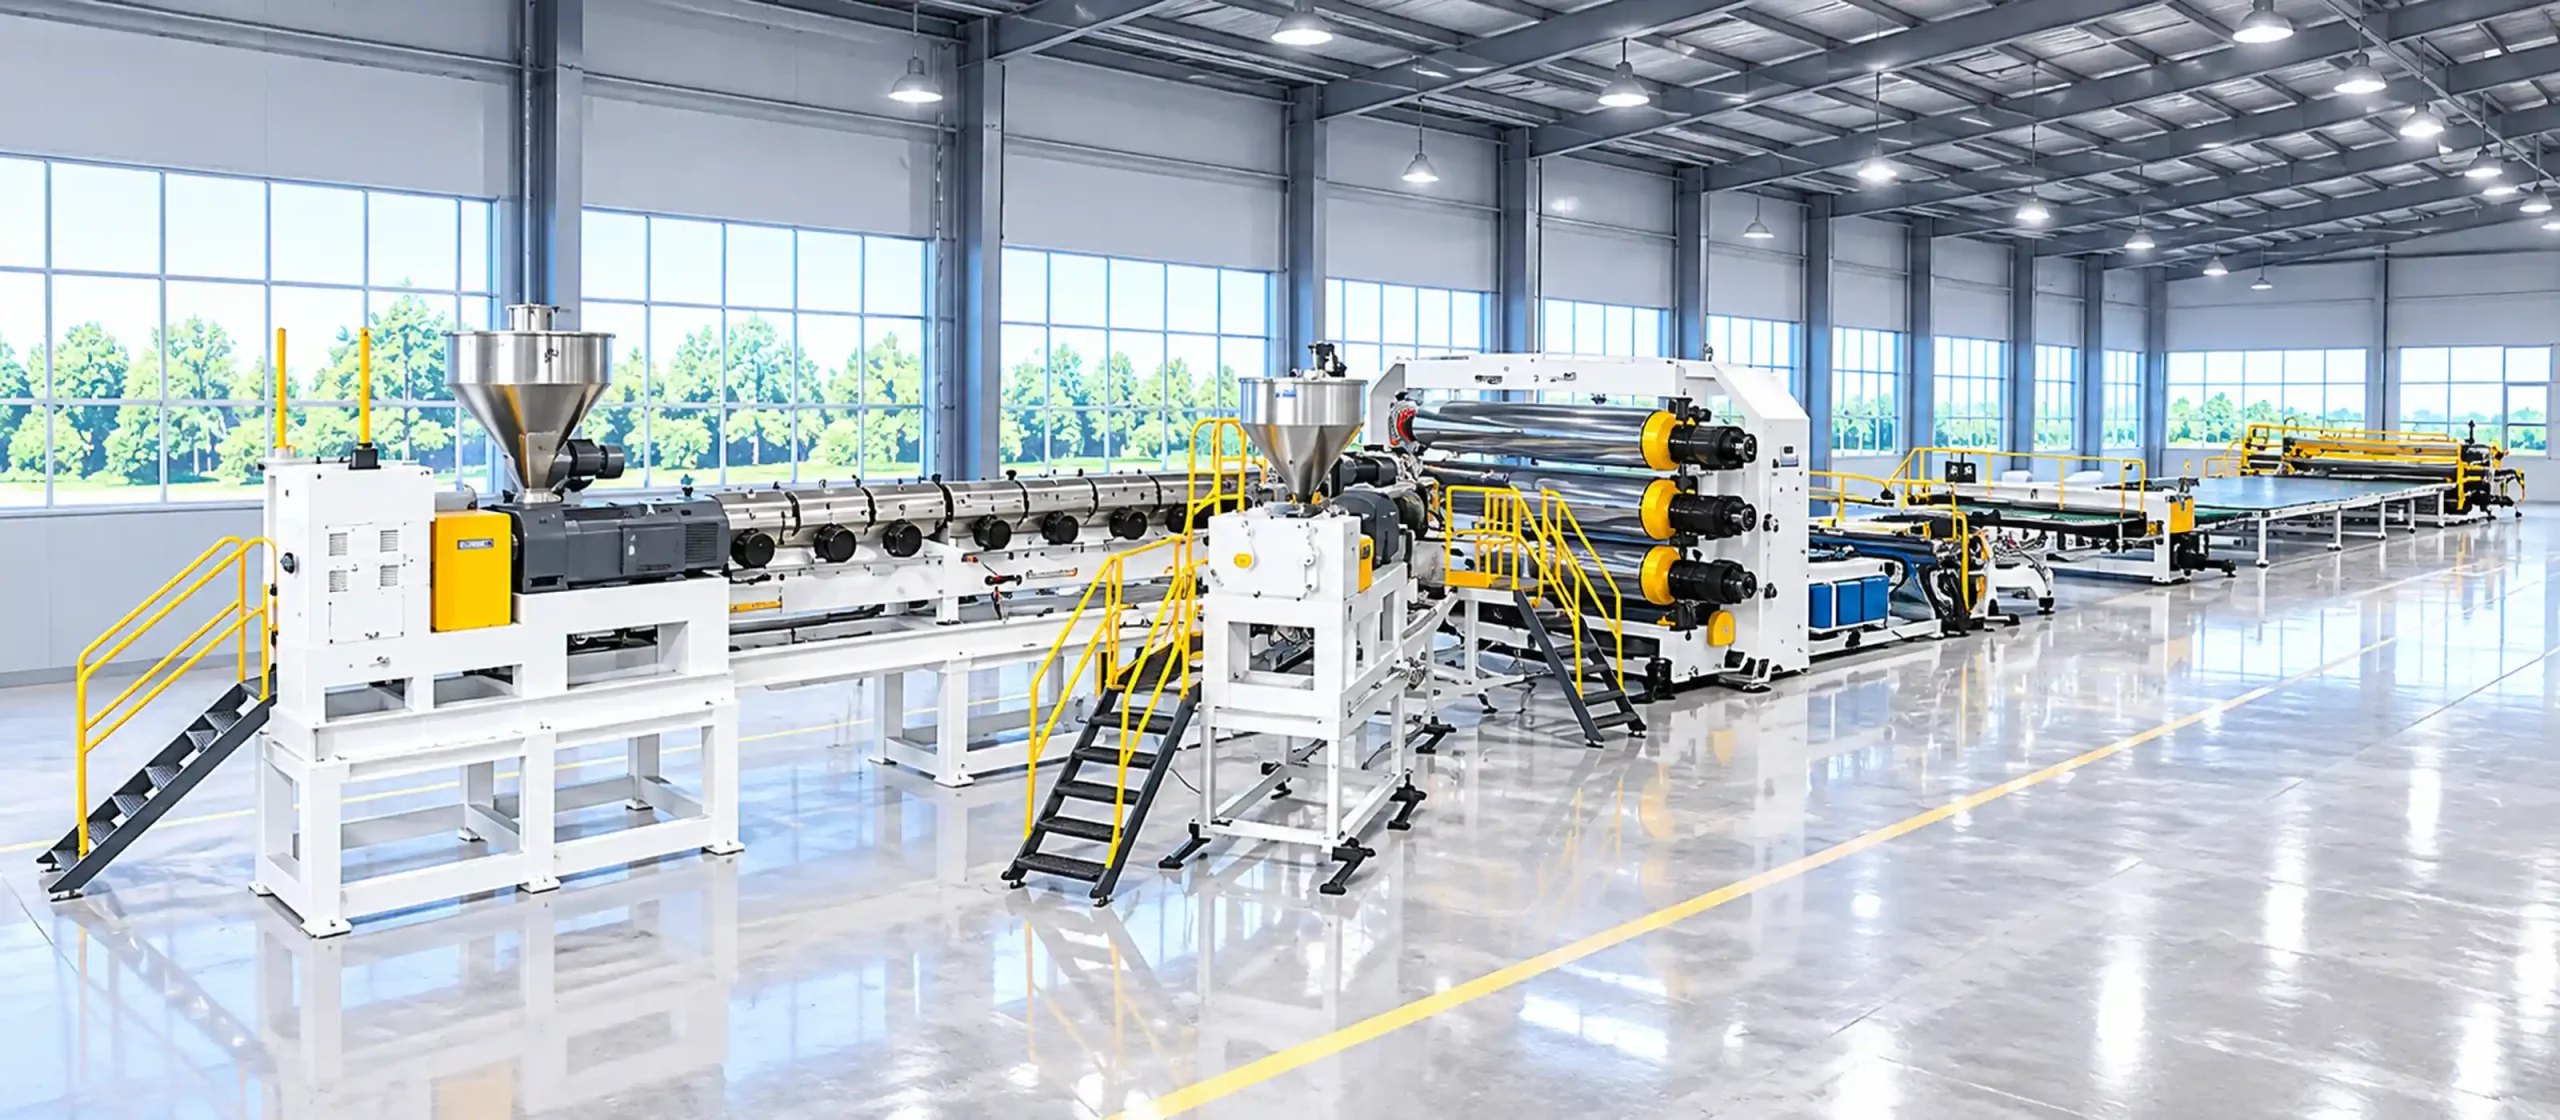
WPC Flooring Production Line
Jwell WPC Flooring Production Line produces lightweight, durable wood-plastic composite flooring with a foamed core, precision calendering, embossing, UV coating and automated profiling.
The PVC Thick Plate Extrusion Line is part of JWELL’s complete extrusion portfolio. Customers evaluating this PVC Thick Plate Extrusion Line also frequently request our PE Thick Plate Extrusion Line | Jwell Machinery and PVC Soft Rigid Sheet Extrusion Line | Jwell Machinery, which share the same proven screw, die and control platforms. For layout drawings, pricing and lead times, contact JWELL Machinery directly.
PVC (polyvinyl chloride) is fundamentally different from polyolefins like PE and PP in one critical aspect: it is thermally sensitive. When PVC is heated above approximately 180°C or held at processing temperature for too long, the polymer chain undergoes dehydrochlorination — releasing HCl gas that is both corrosive to equipment and autocatalytic, accelerating further degradation. The result is discolored, brittle plate with visible burn marks, physical property loss, and corrosive attack on the extruder barrel and screw.
Jwell addresses this fundamental material challenge through dedicated conical twin-screw extruder geometry, available in two configurations:
Model 80/156: Screw diameters 80 mm (feed end) / 156 mm (discharge end). The converging screw geometry compresses the PVC dry blend naturally as it travels from feed zone to metering zone, without the high-shear compression that parallel screws impose. The larger-diameter feed section provides excellent intake of low-bulk-density PVC dry blend powder, while the smaller-diameter discharge section generates the melt pressure needed for die flow at lower screw RPM — and therefore lower shear heating.
Model 92/188: Screw diameters 92 mm / 188 mm. Larger capacity for higher output requirements (400-500 kg/h), with the same conical geometry advantages.
The conical design’s key advantage for PVC is residence time reduction: 30-50% shorter than a parallel twin-screw extruder of equivalent output. This directly translates to reduced thermal history exposure and lower risk of degradation. The screw is manufactured from nitrided steel with 950 HV surface hardness and corrosion-resistant treatment, while the barrel is equipped with bimetallic alloy liners specifically formulated for HCl resistance in PVC service.
The four-zone barrel temperature control (barrel zones 1-4, adapter, die) uses independent PID-controlled ceramic band heaters with closed-loop water cooling on selected zones to pull heat out when the exothermic PVC reaction raises temperature above setpoint — a cooling capability that conventional extruders without water-cooled barrels lack.
PVC melt presents unique challenges for die design that polyolefin die designs do not address. PVC melt tends to adhere to metal surfaces at processing temperature, forming a degraded layer over time that (1) narrows the flow channel, causing progressive plate thickness drift, (2) sheds degraded particles into the melt stream, creating visible black specks on the plate surface, and (3) requires increasingly frequent die cleaning — a 4-8 hour procedure on a poorly designed die.
Jwell’s PVC thick plate T-die is engineered with three PVC-specific features:
Mirror-polish chrome plating on all melt-contact surfaces. The chrome layer provides a non-stick surface that PVC melt slides over rather than adheres to, reducing material stagnation and degradation buildup. Surface roughness below Ra 0.1 μm eliminates the microscopic crevices where PVC melt accumulates and thermally degrades.
Streamlined flow channel geometry designed through computational flow simulation. The coat-hanger manifold is dimensioned to maintain uniform melt velocity from the die center to each side, with the manifold cross-section reducing progressively toward the die edges. Every transition and corner in the flow path is radiused to prevent dead zones where stagnant melt would degrade.
Flexible lip with manual or automatic adjustment. The flexible lip allows the operator to fine-tune plate thickness profile across the web width. Manual adjustment is standard; an automatic die with individual thermal bolts responding to online thickness gauge feedback is available as an upgrade for customers requiring ±1.5% thickness tolerance across the full plate width.
For PVC foam board and free-foam PVC sheet production, the T-die can be equipped with a specialized internal manifold that provides the pressure drop after the die exit required for controlled foaming.
配图建议: T-die 特写,展示铬镀层和柔性唇口 (to be acquired)
Rigid PVC plate surface quality — gloss, flatness, and freedom from cooling marks — is determined by the roll stack in the first 60 seconds after the melt exits the die. If the first roll is too cold, the plate surface quenches instantly, trapping flow lines from the die. If the first roll is too hot, the plate sticks and wraps. If roll temperature is non-uniform (a common problem with simple once-through cooling systems), the plate develops waviness — visible distortion bands caused by differential thermal contraction.
Jwell’s three-roll vertical calibration stack addresses all three surface quality variables through independent temperature control on each roll, maintained by a closed-loop pressurized water circuit with ±1°C uniformity across the full roll face width. The temperature range of 20-90°C covers the full PVC plate calibration window, from rapid-cool thin-gauge plate (3-6 mm) to slow-cool thick plate (12-20 mm) where excessively fast cooling would create internal stress and plate warpage.
The vertical roll orientation — melt enters from above, descends through the gap between rolls 1 and 2, wraps roll 2, then passes between rolls 2 and 3 — provides both-side contact with the calibrating roll surfaces for uniform surface finish on both faces of the plate. Roll diameter is 400 mm, sufficient to provide the contact length needed for thick plate cooling. The chrome-plated roll surfaces accept interchangeable sleeves for mirror, matte, or textured finishes.
The roll gap is servo-adjusted with 0.01 mm precision, calibrated for each plate thickness recipe stored in the PLC.
配图建议: 三辊压光堆特写 (to be acquired)
Unlike polyolefin extrusion where the feedstock is pellets, rigid PVC thick plate production starts from PVC dry blend — a powder mixture of PVC resin, stabilizer, lubricant, impact modifier, processing aid, filler, and pigment — compounded in a high-speed hot mixer and cooled in a cold mixer. The dry blend’s low bulk density (0.45-0.60 g/cm³ versus 0.55-0.65 g/cm³ for pellets), powder flow characteristics, and thermal sensitivity create specific feeding requirements:
Volumetric or gravimetric feeding from a hopper with mechanical agitation (bridge breaker) that prevents the dry blend from arching or bridging in the hopper throat — a common issue with powder feeds. The agitator ensures consistent mass flow into the screw feed zone.
The conical twin-screw’s large-diameter feed section (80 mm or 92 mm) provides the intake volume needed for low-bulk-density powder at the target throughput. A parallel twin-screw of equivalent output would require a larger overall machine simply to accommodate powder feed volume.
Formulation flexibility: The same extruder processes standard rigid PVC (with Ca/Zn or organotin stabilizer), UV-stabilized PVC for outdoor applications, flame-retardant PVC (UL 94 V-0), and calcium-carbonate-filled PVC (up to 20 phr filler loading). The twin-screw’s distributive mixing action ensures uniform dispersion of all formulation components, preventing stabilizer-rich and stabilizer-poor zones that would cause localized degradation.
配图建议: 干混料斗和喂料系统 (to be acquired)
| Parameter | Specification |
| Available Configurations | Model 80/156 (standard) / Model 92/188 (high capacity) |
| Screw Configuration | Conical twin-screw, counter-rotating |
| Parameter | Specification |
| Extruder Type | Conical twin-screw, counter-rotating |
| Screw Diameter (80/156) | 80 mm (feed end) / 156 mm (discharge end) |
| Screw Diameter (92/188) | 92 mm (feed end) / 188 mm (discharge end) |
| L/D Ratio | Application-specific (conical geometry) |
| Screw Material | Nitrided steel, 950 HV surface hardness, corrosion-resistant treatment |
| Barrel Material | Bimetallic alloy liner, HCl-resistant formulation |
| Barrel Heating Zones | 4 zones + adapter + die |
| Heating Type | Ceramic band heaters, PID control |
| Cooling | Water-cooled barrel zones (selected) for heat extraction |
| Drive Motor | AC motor (power model-dependent) |
| Inverter | ABB or equivalent |
| Output Range | 200 – 500 kg/h |
| Parameter | Specification |
| Plate Thickness Range | 3 – 20 mm |
| Plate Width Range | 900 – 1,560 mm |
| Materials | Rigid PVC (standard, UV-stabilized, flame-retardant V-0, CaCO₃-filled), PVC foam board |
| Feedstock | PVC dry blend (powder) from hot/cold mixer system |
| Parameter | Specification |
| Die Type | Coat-hanger manifold, flexible lip |
| Die Width | Model-dependent (matched to plate width) |
| Flow Surface | Chrome-plated, mirror polish, Ra ≤ 0.1 μm |
| Lip Adjustment | Manual (standard) / automatic thermal bolt (optional) |
| Special Configuration | Foam die with decompression manifold (optional) |
| Parameter | Specification |
| Configuration | 3-roll vertical calibration |
| Roll Diameter | 400 mm each |
| Roll Temperature Range | 20 – 90°C |
| Temperature Control | Independent per roll, closed-loop pressurized water |
| Temperature Uniformity | ±1°C across roll face |
| Surface Finish | Chrome-plated, interchangeable sleeve options |
| Roll Gap Adjustment | Servo, 0.01 mm precision |
| Parameter | Specification |
| Cutting System | Transverse cutting saw, synchronized speed |
| Stacking | Automatic counting and stacking |
| Plate Length | 2,000 – 3,000 mm (standard), customizable |
| Parameter | Specification |
| Line Speed (3 mm gauge) | 2 – 4 m/min |
| Line Speed (20 mm gauge) | 0.3 – 0.6 m/min |
| Total Installed Power | 150 – 350 kW (configuration dependent) |
| Control System | Siemens PLC + HMI touchscreen |
| Recipe Storage | Configurable slots, temperature/roll-gap/speed recipes |
| Parameter | Specification |
| Certifications | CE, ISO 9001 |
| Available as | Complete turnkey solution |
| After-Sales | Global engineer certification system, 48-hour spare parts dispatch |
| 文件名 | Alt Text / 场景 |
| PVC thick plate extrusion line SAT.jpg | Jwell PVC thick plate extrusion line — Site Acceptance Test overview at customer facility / SAT整线 |
| PVC thick plate extrusion line extruder.jpg | PVC conical twin-screw extruder at customer facility — close-up during SAT / 挤出机特写 |
| PVC thick plate extrusion line roller SAT.jpg | Three-roll calibration stack during SAT — PVC plate surface quality verification / 三辊压光 |
| PVC thick plate extrusion line cooling bracket SAT.jpg | Cooling and handling section — downstream equipment during SAT / 冷却托架 |
| 卡片 | 产品名称 / 链接 / 关系 |
| 1 | PVC Marble Sheet Extrusion Line / /sheet-extrusion/pvc-marble-sheet-extrusion-line/ / 相同主机平台(锥双) |
| 2 | PP Thick Plate Extrusion Line / /thick-plate-extrusion/pp-thick-plate-extrusion-line/ / 厚板同类产品 |
| 3 | PE Thick Plate Extrusion Line / /thick-plate-extrusion/pe-thick-plate-extrusion-line/ / 厚板同类产品 |
| 4 | PVC Soft/Rigid Sheet Extrusion Line / /sheet-extrusion/pvc-soft-rigid-sheet-extrusion-line/ / PVC 片材系列 |
| # | 字段 / 类型 / 必填 / 说明 |
| 1 | Name / text / ✅ / placeholder: “Your full name” |
| 2 | Email / email / ✅ / placeholder: “your@company.com” |
| 3 | Country / select / ✅ / 200+国家 |
| 4 | Phone / tel / — / 含国际区号 |
| 5 | Company / text / — / placeholder: “Your company name” |
| 6 | Application / select / ✅ / Chemical Tanks / Construction Panels / Industrial Ducting / Laboratory Bench Tops / Multiple / Other |
| 7 | Target Plate Thickness (mm) / select / ✅ / 3-6 / 6-12 / 12-20 / Multiple ranges |
| 8 | Required Output (kg/h) / select / ✅ / <200 / 200-350 / 350-500 / >500 / Not sure |
| 9 | Extruder Configuration / select / — / 80/156 / 92/188 / Not sure |
| 10 | Project Timeline / select / — / Immediate / 1-3 months / 3-6 months / 6-12 months / Information only |
| 11 | Message / textarea / — / placeholder: “Tell us about your production requirements…” |
| — | CAPTCHA / — / ✅ / reCAPTCHA v3 |
| — | Submit / submit / — / “Request Quote & Configuration” |
| # | 检查项 / 状态 |
| 1 | 唯一 H1,含完整产品名 + 核心关键词 / ✅ |
| 2 | H2 技术关键词覆盖: conical twin-screw, PVC thermal sensitivity, 3-20mm, chemical tanks, construction / ✅ |
| 3 | 规格表为 HTML <table> 文本 / ✅ |
| 4 | 所有图片有描述性 alt 属性 / ✅ |
| 5 | 面包屑用 Schema BreadcrumbList / ✅ |
| 6 | FAQ 用 Schema FAQPage (5个Q&A) / ✅ |
| 7 | 产品信息用 Schema Product + 详细 Organization / ✅ |
| 8 | 视频 ×2 分别用 Schema VideoObject / ✅ |
| 9 | Canonical 自引用 / ✅ |
| 10 | Title tag 50-60 chars / ✅ |
| 11 | Meta description 含核心规格数据 + 关键词 / ✅ |
| 12 | Open Graph 完整 / ✅ |
| 信号 | 体现方式 |
| Experience | 锥双挤出 PVC 厚板技术详解、干混料处理经验、SAT 案例照片 |
| Expertise | 锥形双螺杆 PVC 专用设计、镀铬 T-die 防降解、三辊温控校准、PVC 配方处理 |
| Authoritativeness | 29年经验、8大基地、3500+员工、25000+设备、1000+专利、CE+ISO 9001 |
| Trustworthiness | 全球工程师认证体系、48小时备件调度、近50%出口率、120+国家 |
| 检查项 | 目标值 |
| LCP | < 2.5s |
| CLS | < 0.1 |
| INP | < 200ms |
| Mobile-friendly | ✅ |
| 图片格式 | WebP (建议) |
| 文件 | 用途 / 状态 |
| 视频/PVC thick plate extrusion line FAT.mp4 | [D1] FAT 视频 / ✅ 已有 |
| 视频/PVC thick plate extrusion line SAT.mp4 | 备选第二案例视频 / ✅ 已有 |
| 视频/PVC imitation marble sheet extrusion line.mp4 | [D2] 参考视频 / ✅ 已有 |
| 文件 | 用途 / 状态 |
| Case Study/PVC thick plate extrusion line SAT.jpg | [I] SAT整线 / ✅ 已有 |
| Case Study/PVC thick plate extrusion line extruder.jpg | [I] 挤出机特写 / ✅ 已有 |
| Case Study/PVC thick plate extrusion line roller SAT.jpg | [I] 三辊压光 / ✅ 已有 |
| Case Study/PVC thick plate extrusion line cooling bracket SAT.jpg | [I] 冷却托架 / ✅ 已有 |
| 用途 | 优先级 |
| [C] Hero 画廊 — 产线主图 (3张) | 高 |
| [F1] 锥形双螺杆结构示意图 / 挤出机特写 | 高 |
| [F2] T-die 特写(铬镀层、柔性唇口) | 高 |
| [F3] 三辊压光堆特写 | 中 |
| [F4] 干混料斗和喂料系统 | 中 |
| [F5] 不同厚度 PVC 板样品对比 | 中 |
| [F6] 自动切割堆垛系统 | 中 |
| [F7] 电控柜 + 品牌 logo 条 | 低 |
| [H1] 化工储罐应用配图 | 高 |
| [H2] 建筑板材应用配图 | 高 |
| [H3] 工业管道应用配图 | 高 |
| [H4] 实验台面应用配图 | 中 |
| 视频封面图 ×2 (FAT + 参考视频 poster) | 高 |
| 相关产品卡片缩略图 | 中 |
| 目标页面 | 位置 / 锚文本 |
| PVC Marble Sheet Line | [L] Related Products / “PVC Marble Sheet Extrusion Line” |
| PP Thick Plate Line | [L] Related Products / “PP Thick Plate Extrusion Line” |
| PE Thick Plate Line | [L] Related Products / “PE Thick Plate Extrusion Line” |
| PVC Soft/Rigid Sheet Line | [L] Related Products / “PVC Soft/Rigid Sheet Extrusion Line” |
| 来源页面 | 链接上下文 |
| Thick Plate Extrusion Pillar Page | 厚板挤出分类页 |
| PVC Processing Solutions Overview | PVC 加工整体方案页 |
| Chemical Industry Equipment Solutions | 化工设备方案 |
| Construction Materials Manufacturing | 建材制造方案 |
| 维度 | ABS 线 / PVC Thick Plate 线 |
| 挤出机类型 | 单螺杆 (33:1 L/D) / 锥形双螺杆 (80/156, 92/188) |
| 核心材料挑战 | ABS 橡胶相剪切敏感性 / PVC 热敏性 (HCl 释放) |
| Hero 卖点数 | 9 项 / 8 项 |
| 标签页 | 5 个 / 5 个 |
| 功能区块 | 8 个 / 7 个 |
| 视频数 | 2 个 (FAT + 案例) / 2 个 (FAT + 参考视频) |
| 应用场景数 | 4 个 / 4 个(化工/建筑/管道/实验台) |
| 独特区块 | 市场地位区 [J] (300+ 冰箱线) / 材料优势区 [J] (PVC vs 替代材料) |
| 案例素材 | 6 张照片 + 视频 / 4 张 SAT 照片 |
| E-E-A-T 重心 | 市场地位 + 规模验证 / 材料专业技术 + PVC 加工深度 |
| 特色数据 | 90% 市场份额 + 海尔20年 / 锥双优势 + PVC 热敏性解决 |
Rigid PVC’s chemical resistance — excellent to most inorganic acids (sulfuric acid at concentrations up to 80%, hydrochloric acid all concentrations, nitric acid up to 50%), most alkalis (sodium hydroxide up to 50%), salt solutions, and oxidizing agents — makes PVC thick plate the standard material for chemical storage tanks, process vessels, scrubber towers, and electroplating baths in the chemical processing, metal finishing, and water treatment industries.
PVC tank fabrication uses the 6-20 mm thick plates, cut to size and hot-gas or extrusion welded at the joints to form liquid-tight vessels ranging from small day tanks (500-5,000 liters) to large storage silos (20,000-100,000 liters). The welded joint strength of properly fabricated PVC reaches 80-90% of the base material strength, and the joints share the same chemical resistance as the plate itself — unlike lined steel tanks where a liner breach exposes the steel substrate to chemical attack.
PVC plate tanks are self-supporting up to approximately 2 meters sidewall height at 6 mm thickness; taller tanks use thicker plate (12-20 mm) or external steel reinforcement. For outdoor installations, UV-stabilized PVC grades with titanium dioxide pigmentation prevent the surface chalking and embrittlement that affects unpigmented PVC under prolonged sun exposure.
Jwell line capability: The 3-20 mm thickness range directly covers the entire PVC plate spectrum used in chemical tank fabrication — from 6 mm for small vessels to 20 mm for large tank walls. Jwell PVC plate customers supplying the chemical equipment industry can produce the full thickness range for tank fabricators from a single extrusion line.
Rigid PVC thick plate (3-12 mm) is fabricated into a wide range of building and construction products:
– Wall cladding and facade panels: PVC’s inherent water resistance eliminates the moisture-absorption issues of wood, gypsum, and cement-based panels. PVC cladding requires no painting, no sealing, and no periodic maintenance — a lifecycle cost advantage valued in commercial buildings, hospitals, and food processing facilities where hygiene and cleanability are regulatory requirements. UV-stabilized grades retain color and surface integrity after years of direct sun exposure.
– Partition panels and cubicle systems: PVC bathroom partitions, toilet cubicles, and changing room dividers leverage PVC’s water resistance and easy-to-clean surface. The material does not delaminate, swell, or support mold growth in the continuously humid environment that destroys wood-based and MDF partitions within 3-5 years.
– Door panels: Solid PVC plate doors for chemical plants, wastewater treatment facilities, and food processing plants where metal doors corrode and wooden doors rot. PVC doors are fabricated from 6-12 mm plate with internal reinforcing where required.
– PVC foam board: For lower-density applications (signage, exhibition displays, interior decoration), the line also produces PVC foam board using a chemical blowing agent formulation, with density adjustable from 0.4 to 0.8 g/cm³.
Fire safety: Flame-retardant PVC grades meeting UL 94 V-0 are processable on the same line with formulation adjustment. PVC is inherently self-extinguishing due to its chlorine content (approximately 57% by weight), which releases chlorine radicals that quench the combustion reaction in the gas phase. This intumescent fire behavior is a key specification advantage over polyethylene and polypropylene panels in building applications where fire codes apply.
PVC (polyvinyl chloride) is thermally sensitive — it degrades and releases corrosive HCl gas if overheated or held too long at processing temperature. Jwell’s conical twin-screw extruder (80/156 and 92/188 configurations) addresses this through its converging screw geometry, which provides natural compression without excessive shear. The residence time is 30-50% shorter than a parallel twin-screw of equivalent output, minimizing thermal history exposure. Additionally, the larger-diameter feed section handles the low bulk density of PVC dry blend powder (0.45-0.60 g/cm³) more effectively than a parallel screw intake zone. The water-cooled barrel zones extract heat from the exothermic PVC reaction, preventing temperature overshoot beyond the setpoint.
The two model designations refer to the conical twin-screw diameters:
– 80/156: 80 mm feed-end diameter / 156 mm discharge-end diameter. Standard output configuration for 200-350 kg/h production.
– 92/188: 92 mm feed-end diameter / 188 mm discharge-end diameter. Higher-capacity configuration for 350-500 kg/h production.
The larger-diameter feed section on both models provides proportional intake volume for PVC dry blend feeding. Customers select the model based on their target daily output and plate dimensions. Both models share the same conical geometry advantages for PVC processing.
The line produces rigid PVC plates from 3 to 20 mm thickness in widths of 900-1,560 mm. The application range covers:
– 3-6 mm: Chemical tank lining, laboratory bench tops, fume hood panels
– 6-12 mm: Construction panels, wall cladding, partition panels, door panels
– 12-20 mm: Self-supporting chemical tank walls, industrial ducting panels, heavy structural plates
The line also produces PVC foam board using a chemical blowing agent formulation (density 0.4-0.8 g/cm³) and free-foam PVC sheet with appropriate die configuration.
Unlike polyolefin extrusion (PE, PP) where the feedstock is pellets, rigid PVC thick plate production uses PVC dry blend — a free-flowing powder mixture of PVC resin, heat stabilizer, lubricant, impact modifier, processing aid, filler (typically calcium carbonate), and pigment. The dry blend is prepared in a separate hot/cold mixer system upstream of the extruder. The hot mixer heats the blend to 110-120°C through friction, driving the liquid stabilizer and lubricant into the PVC resin particles; the cold mixer then cools the blend to below 40°C to prevent thermal history accumulation before extrusion.
The conical twin-screw extruder’s large-diameter feed section with mechanical bridge-breaker agitation handles the low-bulk-density powder feedstock reliably.
Yes. With a chemical blowing agent (typically azodicarbonamide or sodium bicarbonate) incorporated in the dry blend formulation, the same conical twin-screw extruder produces PVC foam board with apparent density of 0.4-0.8 g/cm³. The T-die for foam production incorporates a decompression zone after the die exit, where the melt pressure drops and the blowing agent decomposes to form the cellular structure. The roll stack configuration is adjusted for the lower-density, thicker foam sheet. Free-foam PVC sheet (Celuka process) uses a specialized die with an internal torpedo that creates the integral skin-foam-core structure.
Jwell WPC Flooring Production Line produces lightweight, durable wood-plastic composite flooring with a foamed core, precision calendering, embossing, UV coating and automated profiling.
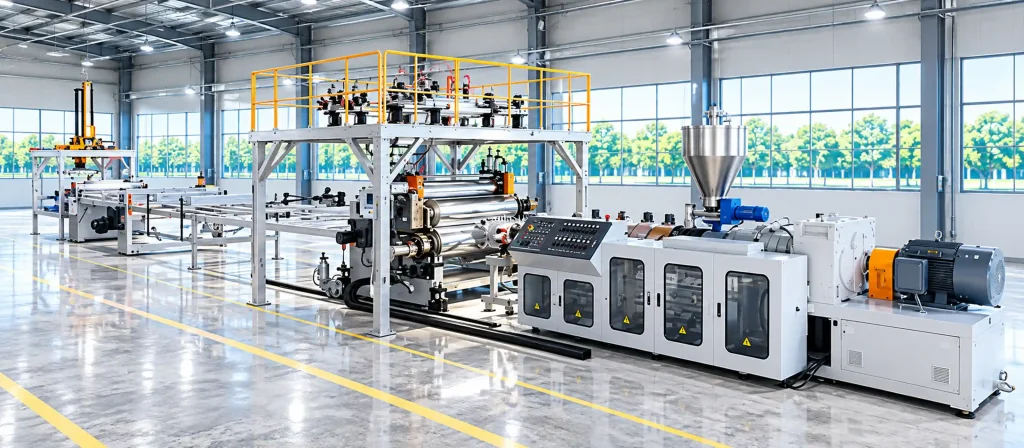
Jwell SPC Flooring Production Line delivers turnkey production from mixing and extrusion to calendering, UV coating, profiling, lamination and packaging.
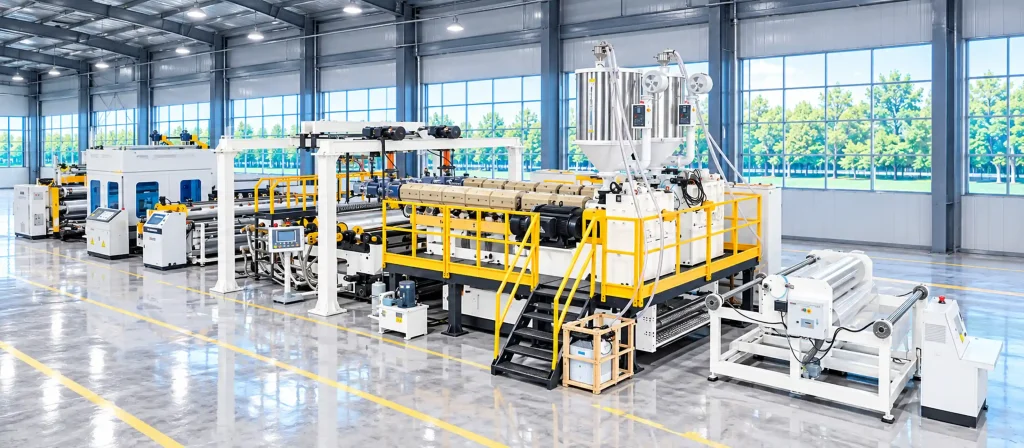
JWELL TPU Casting & Laminating Film Extrusion Line integrates precision casting, online lamination and automatic winding to produce TPU composite films and laminated fabrics for footwear, textiles and outdoor applications.
Jwell Machinery Co., Ltd sets up in 1997 , we are large manufacturer of plastic extrusion machinery in China, our headoffice was located in Shanghai.
SOLUTIONS
PRODUCTS
CONTACT
Copyright © Jwell Machinery Co., Ltd 2026. All rights reserved. Privacy Policy | Terms & Conditions | Site Map
Tell us about your specific requirements. Our team can help you identify a solution for your project.